Automatic storage for chemical facilities with safer handling and better inventory control
Automatic storage in chemical facilities is not just a faster way to move drums, totes, pallets or spare parts. It is a controlled storage approach that combines equipment, software, sensors and operating rules to identify, place, track and retrieve materials with less manual intervention.
For chemical producers, distributors and equipment operators, the strongest use cases are usually safer handling, more reliable inventory data, better use of floor space and fewer routine forklift movements. The limit is just as important: automation does not remove chemical risk. Flammable liquids, corrosives, oxidizers, water-reactive materials and regulated oils still require hazard classification, segregation, containment, ventilation and fire protection before an automated storage design can be considered practical.
This article explains how automatic storage fits into chemical storage systems, which design questions matter, and where automation can create measurable operational value without overstating its role.
What automatic storage means in chemical operations
In industrial warehousing, automatic storage often refers to automated storage and retrieval systems, commonly called AS/RS. MHI describes AS/RS as a combination of equipment and controls that handle, store and retrieve materials with precision, accuracy and speed under a defined degree of automation. In a chemical setting, the same concept can apply to pallet AS/RS, vertical lift modules, shuttle systems, robotic tote storage, automated drum handling, controlled chemical cabinets, conveyor-fed quarantine zones and software-managed bulk storage interfaces.
The common element is not the robot or the crane. It is the controlled loop: the material is identified, assigned to a permitted location, moved by a defined mechanism, recorded in inventory software and retrieved through a traceable request. That loop may be fully automated in a high-bay warehouse, or only partially automated in a smaller plant where operators still load and unload at transfer points.
Chemical facilities should therefore define automatic storage by function rather than by equipment category. A system that reduces search time but allows incompatible materials to be stored together is not a strong chemical storage system. A slower system with verified compatibility rules, spill control and access control may deliver more practical value.
Why chemical storage needs a different automation lens
General warehouses often evaluate automation by throughput, labor availability, picking accuracy and space utilization. Those factors also matter in chemical operations, but the decision must start with material risk. A chemical storage area may contain liquids with different flash points, corrosive packaging, pressure-sensitive containers, temperature limits or environmental reporting obligations. This shifts the main design question from “How fast can the system retrieve?” to “What can be safely stored, where, under what conditions and with what failure response?”
In the United States, OSHA’s 29 CFR 1910.106 addresses flammable liquids in workplace settings, while EPA’s SPCC rule at 40 CFR Part 112 applies to certain facilities that store oil above threshold quantities and require spill prevention planning. NFPA 30 is widely used for flammable and combustible liquid storage practices, including liquid storage rooms, liquid warehouses and fire protection considerations. These references do not make every facility identical, but they show why chemical storage automation must be evaluated against the stored commodity, container type, building design and emergency response assumptions.
Automation can reduce exposure during routine handling. Fewer forklift trips may reduce impact risk, and goods-to-person retrieval can limit climbing, reaching and manual lifting. At the same time, compact automated storage can change fire dynamics, sprinkler access, smoke movement, inspection visibility and emergency access. The NFPA Research Foundation has highlighted automated storage and retrieval system fire protection as an area where system type, vessel material, energy source, load configuration and rack clearances all affect the protection strategy.
Core automatic storage formats used around chemical materials
Pallet AS/RS for drums, bags and packaged products
Pallet AS/RS can be useful where packaged chemical goods move in standardized pallet loads. Stacker cranes or shuttle systems can store pallets in high-density racking and retrieve them for shipping, production staging or quality inspection. The main benefits are better vertical space use, controlled access and reduced vehicle traffic in storage aisles.
Suitability depends on pallet quality, load stability, container integrity, weight distribution and compatibility rules. Drums, intermediate bulk containers and bagged raw materials may behave differently under acceleration, vibration or high-bay storage. If labels, closures or pallets degrade in service, automation can multiply the consequences because the system assumes repeatable load geometry.
Vertical lift modules and carousels for smaller containers
Vertical lift modules and carousel systems are often considered for lab chemicals, maintenance parts, gaskets, valves, instruments and smaller packaged materials. Their value is strongest when many stock keeping units occupy limited space and when access control is important. For chemical use, the system must still account for container compatibility, ventilation, spill trays, maximum allowable quantities and the possibility that some materials should not be enclosed in a standard unit.
Automated tank and bulk storage interfaces
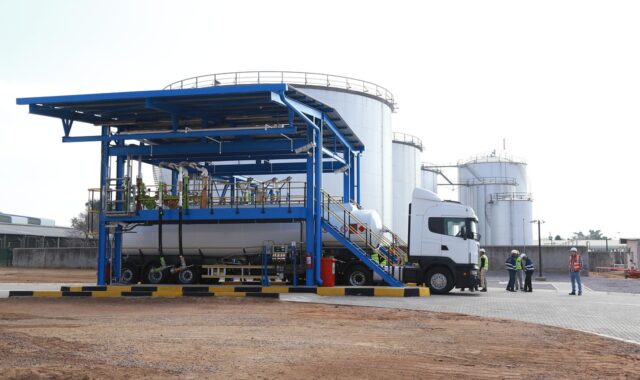
Bulk chemical tanks are not usually described as AS/RS, but they can be part of an automatic storage strategy when level sensors, transfer valves, batch control software and interlocks manage inventory movement. The key difference is that the stored material is not retrieved as a discrete pallet or bin; it is transferred through piping, pumps and controlled discharge points.
For liquid systems, automation should support overfill prevention, line identification, valve status confirmation and alarm response. It should not be used as a substitute for secondary containment, integrity inspection or operator training. EPA SPCC guidance emphasizes inspection and testing programs for bulk storage containers in covered facilities, which is a reminder that instrumentation and software must sit on top of sound mechanical integrity practices.
Safety and compliance questions before layout design
Before choosing cranes, shuttles, conveyors or robots, a chemical operator should complete a structured review of the stored materials and operating constraints. The following questions are more useful than starting with equipment capacity:
- Which materials are flammable, combustible, corrosive, toxic, oxidizing, water-reactive or temperature-sensitive?
- Which containers are used, and are they compatible with automated handling forces?
- Which materials must be segregated from each other under the facility’s safety rules?
- What is the maximum quantity allowed in the proposed room, rack, cabinet or control area?
- How will spills be detected, contained and accessed for cleanup?
- Can emergency responders reach the area if a load jams, leaks or burns?
- Does the fire protection design match the commodity, packaging, rack configuration and storage height?
- What manual override, lockout and maintenance procedures are required?
This review should include environmental health and safety staff, process engineers, warehouse managers, maintenance teams, insurers and the authority having jurisdiction where required. Automatic storage projects fail when they are treated only as material handling investments. In chemical storage, they are also safety, compliance and mechanical integrity projects.
Controls, data and traceability are part of the storage system
The software layer is often where automatic storage delivers its most visible improvement. A warehouse management system or manufacturing execution system can assign storage locations, block incompatible placements, manage first-expired-first-out rules, record lot numbers and produce more reliable inventory counts. Barcode or RFID identification can reduce manual entry errors, while sensors can monitor door status, temperature, humidity, liquid level, vibration or abnormal equipment conditions.
For chemical facilities, data quality is not an administrative detail. Incorrect item master data can send a material to the wrong zone. Missing hazard information can defeat segregation logic. Poor lot control can complicate quality release or recall. If the system connects to production planning, procurement or shipping, a storage error can quickly become a production or customer service problem. See also: Pumps and Valves.
Cybersecurity should also be considered. Automated cranes, shuttles, valves and conveyors depend on control networks. A disruption may not only stop retrieval; it may leave materials in inaccessible locations or interrupt temperature-controlled storage. Facilities should define who can modify storage rules, who can override alarms, how backups are maintained and how the operation continues during a software or power failure.
A practical evaluation checklist for chemical automatic storage
A useful business case should compare automation with the actual constraints of the site, not with a generic warehouse model. The table below summarizes a practical evaluation framework.
| Evaluation area | What to check | Why it matters |
|---|---|---|
| Material profile | Hazard class, container type, weight, temperature range and incompatibilities | Determines whether automation is suitable and where materials may be stored |
| Fire protection | Commodity classification, storage height, rack design, sprinkler arrangement and emergency access | Compact storage can change fire behavior and protection assumptions |
| Containment | Secondary containment, drainage, spill detection and cleanup access | Automated movement does not eliminate leaks or damaged containers |
| Inventory control | Lot tracking, expiry control, quarantine status and system integration | Creates value beyond mechanical movement |
| Maintenance access | Safe entry, lockout, spare parts and recovery from jams | Reduces downtime and protects technicians |
| Operating resilience | Power loss, software outage, manual retrieval and emergency procedures | Ensures storage remains manageable during abnormal events |
The strongest candidates for automatic storage usually share several traits: repeatable container dimensions, stable demand patterns, high value of traceability, limited floor space, frequent retrieval and a need to reduce operator exposure. Weak candidates include damaged or inconsistent pallets, poorly labeled legacy stock, materials requiring frequent manual inspection, or product groups with unresolved compatibility rules.
Where automatic storage creates real value
The most credible value of automatic storage is not a single headline number. It comes from several improvements that reinforce one another. Better location control reduces search time. Fewer open aisles and fewer forklift movements can lower routine traffic risk. Controlled access can limit unauthorized handling. Software-directed retrieval can improve lot rotation and reduce expired stock. Higher storage density can delay building expansion or free space for staging and inspection.
For chemical equipment and process operations, automatic storage can also improve maintenance readiness. Spare seals, pump parts, instruments, filters and safety-critical components can be stored in controlled modules with clearer inventory visibility. This matters because a missing replacement part can extend downtime even when the production chemistry is well controlled.
Automation should not be presented as a universal answer. If a facility has poor housekeeping, weak labeling, outdated safety data, irregular pallets or unclear ownership of storage rules, automation may make problems harder to see. The best projects often begin with data cleanup, packaging standardization, safety review and zone redesign before the first automated machine is installed.
Implementation approach for lower project risk
A phased approach is usually safer than a full-scale conversion. Start with a defined material family, a clear storage zone and measurable objectives such as reducing manual picks, improving count accuracy or separating quarantine inventory. Confirm that container dimensions, labels and pallets are consistent. Test emergency procedures, maintenance access and manual recovery before expanding to higher-risk materials.
Facilities should also involve fire protection engineers early, especially for high-density or high-bay automated systems. The storage technology, rack geometry, ceiling height, in-rack sprinkler needs, packaging materials and stored commodity all influence the protection design. Waiting until equipment selection is complete can lead to expensive redesign or restrictions on what may be stored.
Training remains essential. Operators need to understand not only how to request materials, but also why certain placements are blocked, how to respond to alarms, how to report damaged containers and when to stop the system. Maintenance teams need lockout procedures and safe access plans. Supervisors need reports that show exceptions, overrides, aging stock and blocked inventory, not only throughput.
Frequently asked questions
Is automatic storage the same as AS/RS?
AS/RS is one major form of automatic storage, but the broader term can also include automated cabinets, vertical lift modules, robotic tote systems, conveyor-fed storage, software-controlled bulk tank interfaces and sensor-based inventory control. The best definition depends on what the facility is trying to control.
Can flammable liquids be stored in an automated system?
Potentially, but only after reviewing the liquid classification, container type, quantity, building design, ventilation, containment and fire protection. OSHA rules, NFPA 30 practices, insurer requirements and local authority review may all affect the final design. Automation should not be selected before these constraints are understood.
Does automation reduce chemical storage risk?
It can reduce some risks, especially manual handling, traffic exposure, picking errors and unauthorized access. It can also introduce new risks, such as jam recovery, limited inspection visibility, control system failure and more complex fire protection. The net result depends on design quality and operating discipline.
What should be prepared before requesting an automatic storage proposal?
Prepare a material list with hazard information, container dimensions, pallet standards, movement frequency, storage temperature needs, segregation rules, current incident issues and inventory accuracy goals. Without this information, a proposal may optimize equipment movement while missing the real chemical storage constraints.
What is the main takeaway for chemical facilities?
Automatic storage is most effective when it is treated as an integrated storage system, not just a warehouse machine. The project should connect material compatibility, fire protection, containment, inventory data, maintenance access and emergency response into one design before capacity and speed are optimized.