Pump valves explained for chemical and industrial pumping systems
What pump valves do in a pumping system
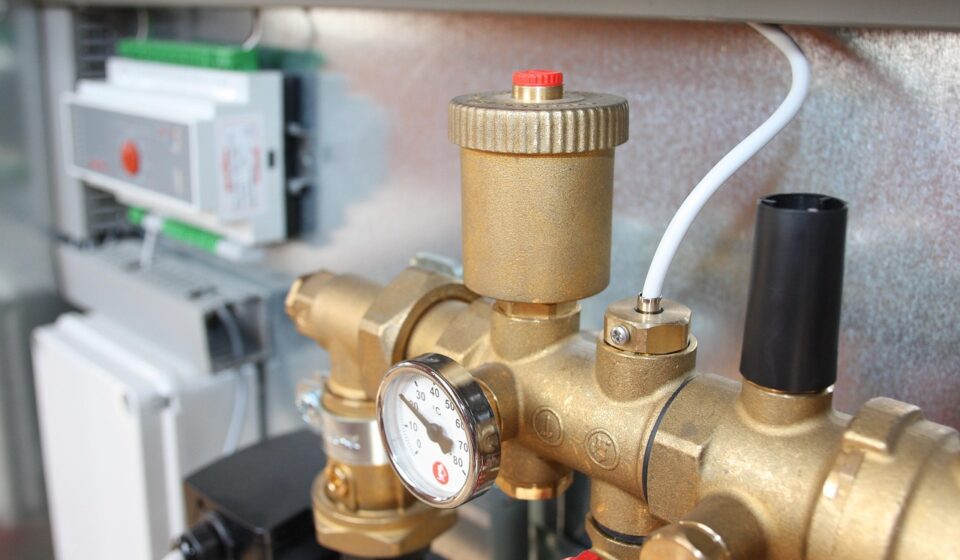
Pump valves are part of the hydraulic design, not simple accessories around the pump. They determine how the pump is isolated, started, protected, controlled and maintained. In chemical and industrial systems, a poor valve arrangement can increase pressure loss, reduce net positive suction head margin, create water hammer, allow reverse flow or make maintenance unsafe. Each valve should have a defined duty: isolation, non-return protection, throttling, pressure relief, bypass, draining, venting or instrumentation. This article looks at pump valves as part of the wider system, rather than as stand-alone components, for readers comparing equipment in the Pumps and Valves field.
A pump adds energy to a fluid. Valves determine where that fluid can go, how much resistance the pump sees and how the system responds when operating conditions change. A small valve symbol on a piping diagram can therefore have a large effect on reliability. A nearly closed discharge valve can move a centrifugal pump away from its efficient operating range. A restrictive suction valve can raise cavitation risk. A missing or poorly selected check valve can allow reverse rotation after shutdown. A positive displacement pump without adequate pressure relief can face dangerous overpressure if discharge flow is blocked.
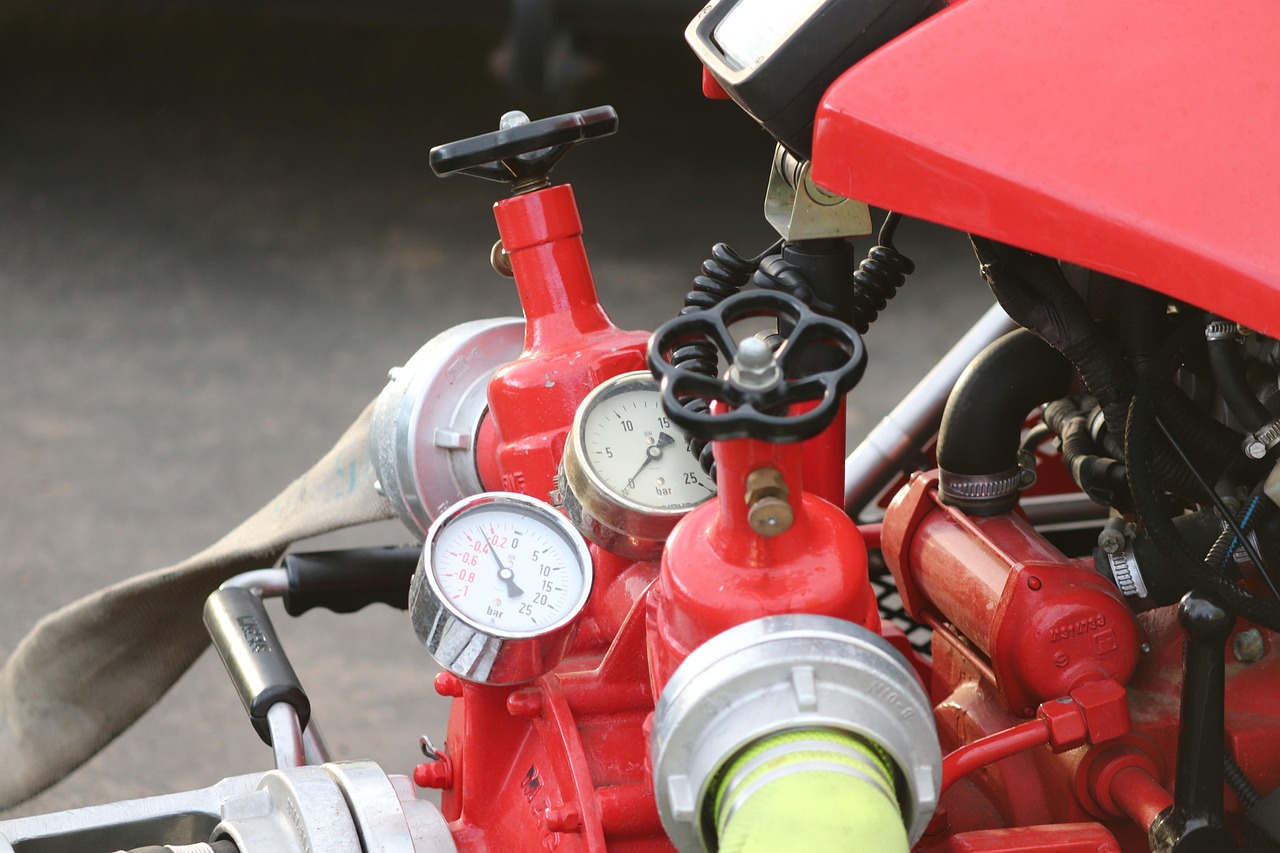
For chemical service, pump valves also carry safety and environmental responsibilities. Corrosive, toxic, hot, volatile or abrasive fluids require careful review of body material, trim material, seat design, stem sealing, end connection, leakage class and maintenance access. The best choice is not simply the lowest-cost valve with the correct nominal size. It is the valve that can perform its required function under the actual pressure, temperature, flow, chemical and operating-cycle conditions of the system.
Common pump valve types and where they fit
Most pump systems use several valve types in combination. The table below summarizes common pump valve duties and the selection issues that normally require attention.
| Valve type | Typical location | Main duty | Key selection notes |
|---|---|---|---|
| Gate valve | Suction or discharge isolation | Full-open or full-closed isolation | Low pressure drop when fully open, but not intended for frequent throttling. |
| Ball valve | Small-bore isolation, chemical lines, drains and vents | Fast shutoff | Good shutoff in many services; material and seat compatibility are critical. |
| Butterfly valve | Medium and large water or utility lines | Isolation and sometimes control | Compact and economical, but disc position and pressure drop must be considered. |
| Globe valve | Discharge or bypass lines | Manual throttling | Better for throttling than gate valves, but usually higher pressure drop. |
| Control valve | Usually downstream of the pump | Automatic flow, level or pressure control | Requires sizing for pressure drop, cavitation, flashing, rangeability and actuator response. |
| Check valve | Discharge side | Prevent reverse flow | Must close reliably without excessive slam, chatter or head loss. |
| Pressure relief valve | Discharge of positive displacement pumps or protected sections | Overpressure protection | Set pressure, relieving capacity and return destination must be engineered. |
| Minimum-flow or bypass valve | Discharge recirculation line | Maintain minimum pump flow | Used where low-flow operation can overheat or damage the pump. |
A common basic arrangement for a centrifugal pump includes a suction isolation valve, a discharge check valve and a discharge isolation valve. If the process requires variable flow, a control valve or variable speed drive may be added, depending on the control method and operating profile. A bypass or minimum-flow line may be required when the pump can run below its safe flow range.
Positive displacement pumps need different protection logic. Because they move a fixed volume per cycle or revolution, blocking the discharge can cause a rapid pressure rise. In these systems, a relief valve, pressure-limiting device or properly engineered bypass is not optional. It is part of safe design.
Selection factors for chemical duty
In chemical equipment, valve selection starts with the service data. Concentration, temperature, solids content, vapor pressure, crystallization tendency, viscosity and toxicity all affect the decision. A valve that performs well in clean cooling water may be unsuitable for hydrochloric acid, sodium hydroxide, solvent transfer, polymer slurry or high-temperature heat-transfer fluid.
Material compatibility should include the pressure-containing body, wetted trim, seat, stem, packing, gasket and bolting environment. Stainless steel, duplex stainless steel, alloy materials, lined valves and engineering plastics all have application limits. For lined valves, the liner must resist permeation, swelling and mechanical damage. In abrasive slurry service, erosion at seats, discs and flow restrictions can become the main failure mode.
Pressure and temperature ratings require more than a nameplate check. ASME B16.34 is widely referenced for flanged, threaded and welding-end valves and covers pressure-temperature ratings, dimensions, tolerances, materials, nondestructive examination, testing and marking for applicable valve constructions. In practice, engineers still need to confirm the exact edition, material group, pressure class, end connection and project code requirements before procurement.
Control valves require a separate sizing review. IEC 60534-2-1:2011 provides equations used for predicting flow through control valves for compressible and incompressible fluids. For pump systems, the practical point is that a control valve should not be selected by line size alone. The specified flow coefficient, available pressure drop, fluid vapor pressure, cavitation or flashing potential, noise, actuator action and fail position should all be checked.
For pumps in petroleum, petrochemical and natural gas industries, API Std 610 is often relevant to the pump specification. Public standards listings identify a thirteenth edition dated June 2026, while many installed assets and active projects may still reference earlier editions such as the twelfth edition from January 2021. That does not automatically determine valve selection, but it can affect overall pump package requirements, test expectations and project documentation. Procurement documents should state the required edition instead of assuming all parties are using the same one.
How valve choices affect efficiency and reliability
Every valve adds resistance to a piping system. In a centrifugal pump system, that resistance becomes part of the system curve. When a discharge valve is throttled, the pump operates against higher backpressure and flow usually decreases. This may be acceptable for simple control, but it can waste energy if the process spends long periods at reduced flow.
The U.S. Department of Energy has long emphasized a system-level approach to pump efficiency, including the reduction of unnecessary pipe and valve pressure losses. This matters because a pump may perform well on a test stand while the installed system still consumes excess energy due to avoidable restrictions, poor control philosophy or operation far from the intended duty point.
The Hydraulic Institute’s ANSI/HI 9.6.3-2024 guideline addresses preferred and allowable operating regions for rotodynamic pumps and the effects of operating away from the best efficiency point. In practical terms, valve decisions should support stable operation near the intended range whenever possible. Continuous operation at very low flow, excessive recirculation or unstable control valve behavior can increase vibration, heat generation, seal stress and bearing load.
Suction-side valves need particular care. A valve on the suction line is often required for maintenance isolation, but it should normally remain fully open during operation. Excessive suction restriction reduces the pressure available at the pump inlet and can reduce the margin between available and required net positive suction head. That margin is central to cavitation avoidance. Cavitation can cause noise, vibration, pitted impellers, reduced capacity and shorter seal life.
Check valves also influence reliability. If a check valve closes too slowly, reverse flow can develop before closure, increasing the chance of slam. If it is oversized or installed in a low-flow condition, it may chatter and wear. If it has high head loss, it becomes a permanent efficiency penalty. Selection should consider flow range, orientation, closing characteristic, maintenance access and compatibility with the pumped fluid.
Typical pump valve arrangements
There is no single arrangement that suits every pump, but several patterns are common in industrial plants. See also: Storage Systems.
Centrifugal transfer pump
A typical clean-liquid transfer pump may use a full-bore suction isolation valve, a discharge check valve, a discharge isolation valve and pressure instruments on the suction and discharge sides. If the pump feeds a controlled process, a downstream control valve may regulate flow or pressure. If there is a risk of operation below the pump’s minimum continuous stable flow, a recirculation or minimum-flow line should be considered.
Chemical metering or dosing pump
A chemical dosing pump may include suction isolation, a suction strainer or calibration column where appropriate, discharge isolation, a back-pressure valve, a pressure relief valve, a pulsation dampener and an injection check valve. Compatibility with concentrated chemicals and safe maintenance isolation are central concerns. For hazardous chemicals, double isolation, drain points and containment strategy may be required by the project safety review.
Cooling water or utility pump
Large utility systems often use butterfly valves for isolation because they are compact and cost-effective at larger diameters. Even so, disc position, actuator torque and pressure loss should be checked. In variable-flow systems, valve authority and pump speed control should be coordinated so control valves are not forced to absorb excessive pressure for long periods.
Slurry or wastewater pump
Slurry and wastewater services put extra stress on seats, discs and small passages. Valve designs with narrow flow paths may clog or erode. Full-port ball valves, knife gate valves, plug valves or specialized check valves may be considered depending on solids size, concentration, settling tendency and maintenance practice. The goal is not only shutoff, but predictable operation after exposure to solids.
Specification checklist for pump valves
A useful pump valve specification converts operating requirements into verifiable details. At minimum, the following items should be defined before purchase:
- Fluid name, concentration, density, viscosity, vapor pressure and solids content.
- Normal, minimum and maximum flow rate.
- Normal and maximum pressure at the valve location.
- Operating and design temperature.
- Valve function: isolation, check, throttling, automatic control, relief, bypass, vent or drain.
- Required shutoff performance and acceptable leakage.
- Body, trim, seat, packing and gasket materials.
- End connection, pressure class and face-to-face requirements.
- Manual, pneumatic, electric or hydraulic actuation requirements.
- Fail-open, fail-closed or fail-in-place action for actuated valves.
- Testing, inspection, documentation and marking requirements.
- Maintenance access, removal clearance and spare parts strategy.
Factory and field testing should be viewed in context. ANSI/HI 14.6-2022 addresses hydraulic performance acceptance testing for rotodynamic pumps, including performance, net positive suction head and hydrostatic pressure testing, as well as recording and reporting of test results. However, a factory pump test does not prove that the installed piping and valve arrangement is efficient. Field verification should compare actual flow, pressure, vibration, valve position and control stability with the design intent.
During commissioning, operators should record the normal positions of manual valves and the normal travel range of control valves. A control valve that is nearly closed during normal operation may indicate excessive pump head, an oversized pump, an oversized valve or an unsuitable control strategy. A check valve that chatters may indicate oversizing, low flow or installation conditions that prevent stable closure. These observations are useful diagnostic signals, not minor annoyances.
Frequently asked questions
Are pump valves part of the pump?
Usually, pump valves are part of the piping or pump package rather than the pump hydraulic element itself. They work with the pump to isolate, protect and control the system. In packaged equipment, some valves may be supplied on a skid, but they still need to be specified for the actual service conditions.
Which valve should be installed on the suction side of a pump?
A suction isolation valve is common so the pump can be maintained without draining the whole system. It should be selected for low pressure drop and should normally remain fully open during operation. Throttling on the suction side of a centrifugal pump is generally avoided because it can reduce inlet pressure and increase cavitation risk.
Can pump flow be controlled with a valve?
Yes. Centrifugal pump flow is often controlled by a downstream throttling or control valve. This can be simple and reliable, but it may waste energy if the pump frequently operates far from the required duty. For variable-demand systems, engineers often compare valve control with variable speed control, impeller trimming or parallel pump operation.
Why is a check valve used after a pump?
A discharge check valve helps prevent reverse flow when the pump stops or when another pump in parallel is operating. This protects against reverse rotation, unwanted backflow and some transient events. The check valve must be selected for the actual flow range to avoid slam, chatter and unnecessary pressure loss.
Do positive displacement pumps need special valve protection?
Yes. Positive displacement pumps can generate high pressure quickly if the discharge is blocked. A relief valve or another engineered overpressure protection method should be included unless the pump design already incorporates suitable protection and the full system has been reviewed.
Key takeaway
The most reliable pump valve arrangement treats the pump, valves, piping and controls as one hydraulic system. Isolation valves make maintenance possible, check valves prevent reverse flow, control valves shape process response and relief or bypass valves protect equipment during abnormal conditions. For chemical and industrial service, the final decision should be based on fluid compatibility, pressure-temperature rating, operating range, control method, inspection requirements and safety review. This reduces the risk of choosing a valve that fits the pipe but fails the process.