Equipment for welding in process equipment fabrication
What equipment for welding must cover in process equipment work
In chemical and other process-industry plants, equipment for welding is not limited to a welding machine and a helmet. It is a controlled work system that may include power sources, torches, gas supply, clamps, positioners, cutting and beveling tools, preheat equipment, ventilation, fire protection, personal protective equipment, inspection instruments, and documentation controls. The right package depends on the material, thickness, joint design, service condition, access, and governing code. For pressure vessels, process piping, tanks, skids, and heat exchanger components, poor equipment selection can affect weld quality, worker safety, inspection results, and long-term reliability. This guide focuses on practical selection for fabrication and repair environments in the Process Equipment field.
Start with the welding duty, not the machine
A common mistake is to choose a welding power source first and define the job later. In process equipment fabrication, the decision should start with the duty. A shop building carbon steel support frames has different needs from a crew repairing stainless process piping in a congested plant area. A pressure vessel nozzle, a storage tank shell seam, a heat exchanger channel, and a pipe spool may all involve welding, but they place different demands on joint preparation, heat input, access, inspection, and traceability.
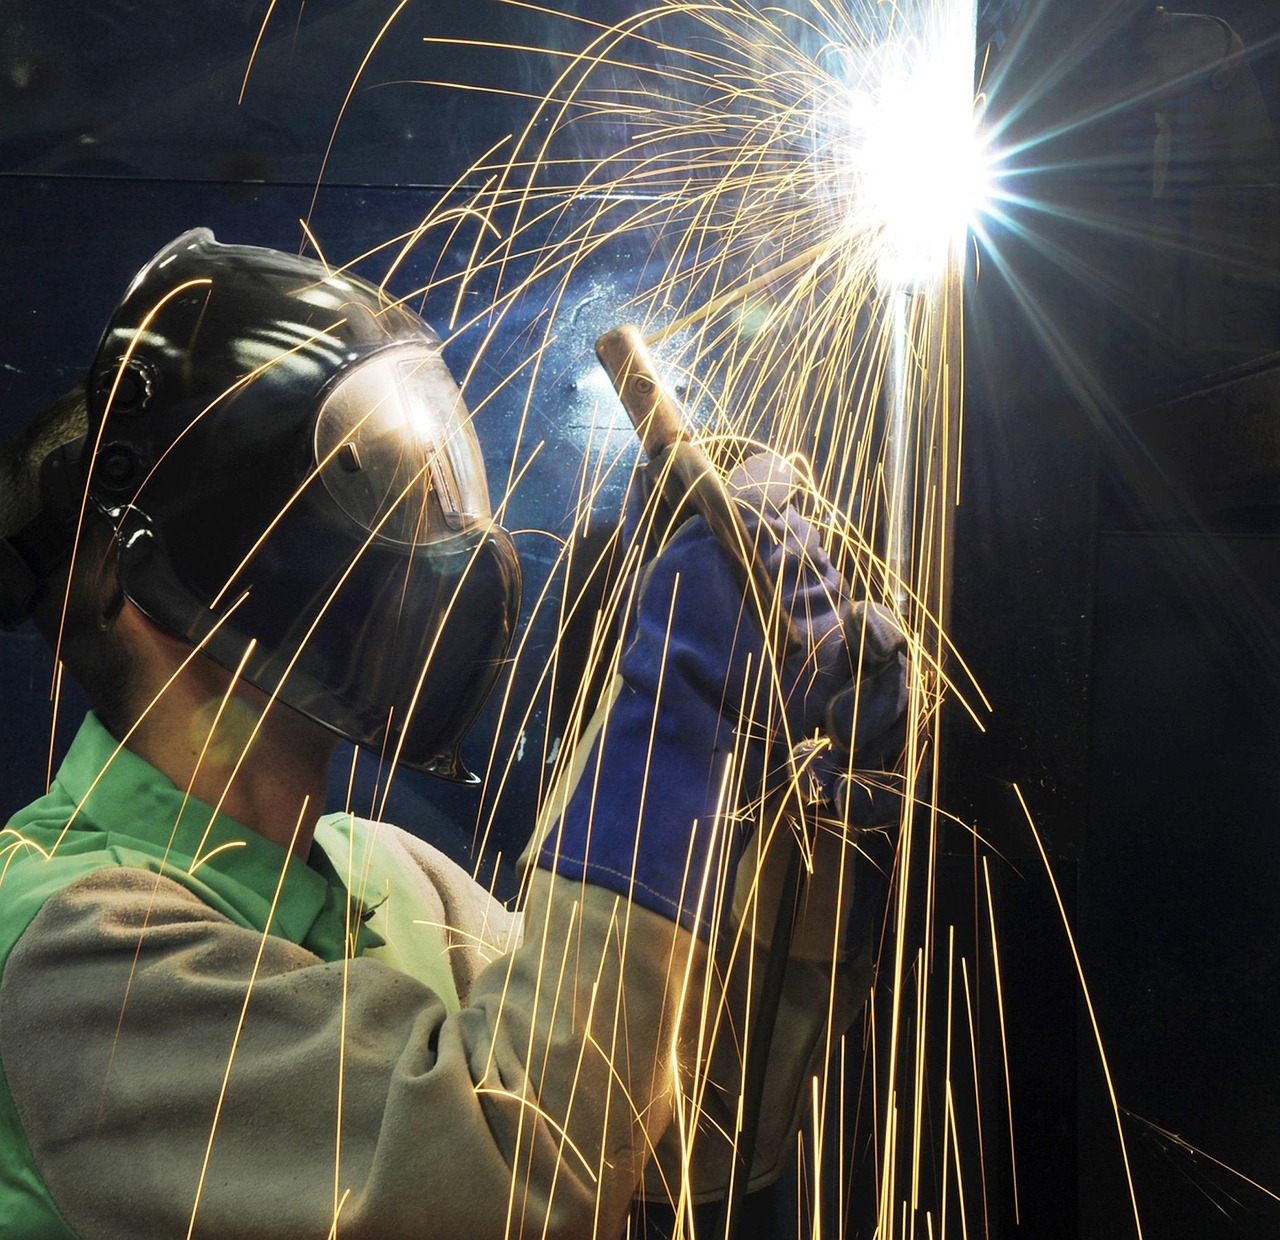
Before specifying equipment, define at least six conditions. First, identify the base material, such as carbon steel, low alloy steel, stainless steel, duplex stainless steel, nickel alloy, aluminum, or clad material. Second, confirm the thickness range and joint type. Third, decide whether the work is shop fabrication, field installation, maintenance repair, or emergency hot work. Fourth, check whether the weld is pressure-retaining, structural, sanitary, corrosion-critical, or non-critical. Fifth, confirm the governing code or project specification. Sixth, consider hazards from flammable residues, confined spaces, coatings, fumes, weather, and electrical conditions.
This front-end definition helps prevent both underbuying and overbuying. A compact inverter may be practical for field SMAW repair, while a submerged arc system can improve productivity on long, repeatable shop seams. A high-quality GTAW setup may be slower, but it is often used where root quality, control, and cleanliness matter more than deposition rate. The equipment is correct only when it supports the weld procedure and the service risk.
Core welding equipment packages and where they fit
The following comparison is a practical way to organize equipment for welding in process equipment fabrication. The table is not a code requirement. It is an engineering selection framework that should be checked against the project welding procedure specification and applicable standard.
| Welding process | Typical equipment package | Common process equipment use | Key limitation to manage |
|---|---|---|---|
| SMAW, or shielded metal arc welding | Constant-current power source, electrode holder, work lead, covered electrodes, electrode oven where required | Field repair, structural attachments, outdoor work, maintenance welding | Manual skill dependence, slag removal, lower productivity on long repetitive seams |
| GTAW, or gas tungsten arc welding | Power source, TIG torch, tungsten electrodes, filler rod, shielding gas, flowmeter, purge equipment | Stainless piping roots, thin wall parts, corrosion-sensitive joints, high-control welds | Lower deposition rate and high sensitivity to cleanliness and shielding |
| GMAW and FCAW | Constant-voltage power source, wire feeder, gun, shielding gas or flux-cored wire, contact tips, drive rolls | Skids, frames, tanks, shop assemblies, medium-thickness components | Wind sensitivity for gas-shielded work, parameter control, spatter and access issues |
| SAW, or submerged arc welding | Power source, travel carriage or manipulator, wire feed, flux delivery and recovery, seam tracking | Long straight seams, heavy plate, pressure vessel shells, tank fabrication | Limited positional flexibility and less suitability for cramped field joints |
| Oxy-fuel, plasma, or thermal cutting equipment | Gas cylinders or supply manifold, regulators, hoses, torch, flashback protection, cutting table or guide | Cutting, gouging, heating, fit-up, removal of old components | Fire risk, gas handling requirements, heat-affected edges that may need preparation before welding |
Many fabrication shops need more than one welding process. A pressure vessel shell may use SAW for long seams, GTAW for certain root passes or small bore connections, and SMAW or FCAW for attachments. A piping job may combine GTAW roots with SMAW, GMAW, or FCAW fill and cap passes, depending on material, location, productivity targets, and the qualified procedure. The practical question is not which process is better in general, but which combination can produce repeatable welds under the actual job constraints.
Supporting equipment that often controls weld quality
The welding arc receives most of the attention, but many weld defects begin before the arc is struck. Joint preparation equipment is one example. Pipe beveling machines, plate edge milling, grinders, burr removal tools, alignment clamps, and fit-up gauges help control root gap, land, bevel angle, and mismatch. If preparation varies from joint to joint, even a capable welder and a high-end power source may produce inconsistent results.
Workholding and positioning are just as important. Positioners, turning rolls, column-and-boom manipulators, rotators, strongbacks, clamps, and tack welding aids reduce awkward body positions and help keep travel speed, electrode angle, and joint access consistent. In process equipment shops, this affects both quality and productivity because cylindrical shells, nozzles, flanges, and pipe spools are rarely as convenient as flat test coupons.
Gas handling also needs careful selection. GTAW and GMAW require reliable shielding gas flow, clean hoses, suitable regulators, flowmeters, and protection against drafts. Stainless steel, duplex stainless steel, and nickel alloy piping may also require internal purge dams, backing gas, purge monitors, and oxygen control according to the written procedure. For corrosion-resistant service, poor shielding can damage the root surface and create later corrosion risk.
Heat control equipment should be treated as part of the welding package, not as an afterthought. Preheat torches, electrical resistance heaters, induction heaters, temperature-indicating crayons, contact pyrometers, infrared thermometers, thermocouples, and chart recorders may be required depending on material and procedure. Some pressure equipment also needs postweld heat treatment using calibrated controls and documented temperature records. These items are not optional accessories when the code, material, or procedure requires a controlled thermal history.
Safety systems are part of the welding equipment package
Welding equipment selection must include safety equipment because process plants create hazards that are not always present in a training booth. In the United States, OSHA 29 CFR 1910 Subpart Q addresses welding, cutting, and brazing in general industry, including general requirements, oxygen-fuel gas welding and cutting, arc welding and cutting, and resistance welding. NFPA 51B is widely used as a fire-prevention reference for welding, cutting, and other hot work. NIOSH guidance also emphasizes that welding fumes can contain complex metal and gas by-products, and that exposure depends on the process, base metal, filler, coating, ventilation, and work duration.
A practical welding safety package should include correctly rated helmets and filter lenses, gloves, flame-resistant clothing, safety glasses, face shields for grinding, hearing protection, respiratory protection where required, welding screens, insulated tools, and suitable footwear. For plant work, also consider gas detectors, lockout and isolation equipment, confined space entry controls, fire blankets, fire extinguishers, spark containment, and hot work permit materials. If the job involves vessels, tanks, or piping that previously contained chemicals, cleaning, isolation, atmospheric testing, and permit control are as important as the welding machine itself.
Gas cylinder and hose management need particular attention. Oxygen-fuel systems require approved apparatus, suitable regulators, compliant hoses, leak control, flashback protection where specified by site rules, and strict separation from oil or grease contamination. Damaged hoses, worn connections, and improvised regulators are unacceptable in process environments because a small equipment fault can quickly become a fire, explosion, or toxic exposure event.
Qualification, inspection, and traceability tools
Process equipment welding is often governed by project codes and standards rather than shop preference alone. ASME B31.3-2024 is a major reference for process piping in chemical, petroleum, pharmaceutical, hydrogen, semiconductor, cryogenic, and related plants. ASME Boiler and Pressure Vessel Code Section VIII is used for many pressure vessel construction projects, while ASME BPVC Section IX covers qualification of welding, brazing, and fusing procedures and personnel for ASME applications. AWS D1.1/D1.1M:2025 covers structural steel welding when it is specified for platforms, supports, frames, or other structural work. API 650 is commonly associated with welded tanks for oil storage. ISO 15614-1:2017 is an international reference for welding procedure qualification tests for arc and gas welding of steels and arc welding of nickel and nickel alloys.
These references do not mean every job uses every standard. They mean the equipment package must support the specified code path. If a weld procedure requires controlled amperage, voltage, travel speed, preheat, interpass temperature, filler classification, shielding gas, or heat treatment, the shop needs tools to control and record those variables. If the project requires welder performance qualification, procedure qualification records, material traceability, or calibrated inspection equipment, those records become part of the fabrication system. See also: Storage Systems.
Inspection equipment may include visual inspection tools, weld gauges, borescopes, dye penetrant materials, magnetic particle equipment, ultrasonic testing instruments, radiographic testing arrangements, hardness testers, ferrite meters, positive material identification equipment, pressure test hardware, and leak test tools. Not all are needed on every job, and some require qualified personnel or specialist contractors. The key point is that inspection planning should happen before production begins, not after welds are already complete.
A practical checklist for selecting equipment for welding
The checklist below adds a verifiable decision layer to purchasing or job planning. It connects the equipment list to service conditions, codes, safety, and inspection rather than treating welding as a stand-alone trade activity.
| Selection question | Why it matters |
|---|---|
| What component is being welded? | Pressure boundary welds, structural welds, tank seams, and temporary attachments may follow different rules. |
| What material and thickness range are involved? | Material controls filler choice, heat input limits, preheat, purge, and postweld heat treatment needs. |
| Which code, edition, and project specification apply? | Equipment must support the required WPS, PQR, welder qualification, inspection, and documentation. |
| Is the work in a shop or operating plant? | Field work may require portable power, weather protection, hot work permits, ventilation, gas testing, and access planning. |
| What joint preparation is required? | Bevel quality, cleanliness, alignment, and fit-up often determine whether welding parameters can be repeated. |
| How will heat be controlled? | Preheat, interpass temperature, heat input, and postweld heat treatment may affect cracking risk and mechanical properties. |
| How will weld quality be verified? | Visual inspection, NDE, pressure testing, and records should be planned with the fabrication sequence. |
| What hazards are present? | Fumes, confined spaces, flammable residues, oxygen-fuel gases, electrical shock, and fire exposure change the equipment package. |
Common selection mistakes to avoid
The first mistake is assuming that higher amperage automatically means a better welding setup. Power capacity matters, but it does not replace procedure control, stable wire feeding, correct polarity, clean gas delivery, or qualified personnel. A powerful machine used with poor fit-up and weak documentation may create more rework than a smaller system matched to the job.
The second mistake is ignoring consumable control. Electrodes, filler metals, fluxes, contact tips, tungsten, backing gas, and purge materials must be compatible with the base metal and procedure. Storage conditions can also matter, especially for low-hydrogen electrodes and moisture-sensitive consumables. Consumable control is part of equipment selection because ovens, quivers, dry storage, labeling, and issue records may be needed.
The third mistake is treating field welding as shop welding with a longer extension cable. Field work often brings wind, poor access, uncertain cleanliness, live plant interfaces, electrical constraints, and fire exposure. Portable screens, weather shelters, gas flow protection, compact positioners, ventilation, lighting, and permit equipment can determine whether a field weld is practical and safe.
The fourth mistake is separating safety from productivity. Good ventilation, positioning, lighting, and access can improve both exposure control and weld consistency. Similarly, a well-organized hot work area can reduce delays because workers do not have to stop repeatedly to correct preventable hazards.
Frequently asked questions
What is the basic equipment for welding?
Basic equipment includes a suitable power source, electrode holder or torch, work lead, cables, filler material, shielding gas equipment when required, cleaning tools, clamps, PPE, and fire protection. In process equipment work, the basic package often expands to include joint preparation tools, preheat equipment, ventilation, gas testing, inspection gauges, and documentation controls.
Which welding equipment is commonly used for stainless steel process piping?
GTAW equipment is commonly used for stainless steel root passes because it provides strong control over the weld pool and shielding. Depending on pipe size, wall thickness, service, and procedure, fill and cap passes may use GTAW, SMAW, GMAW, or FCAW. Purge equipment and oxygen control can be critical for internal root quality.
Is oxy-fuel equipment still useful in process equipment fabrication?
Yes. Oxy-fuel equipment is still used for cutting, heating, fit-up, and some maintenance tasks, although plasma cutting, mechanical cutting, and other methods may be preferred for certain materials or precision requirements. In plant environments, oxy-fuel use requires careful gas handling, hose inspection, fire prevention, and permit control.
Can one welding machine cover all process equipment jobs?
One multiprocess machine can cover many maintenance and light fabrication tasks, but it usually cannot replace a complete process-specific setup. Heavy vessel seams, stainless piping, tank fabrication, structural steel, and corrosion-resistant alloy work may need different torches, wire feeders, shielding systems, positioners, heat controls, and inspection plans.
How does welding equipment affect inspection results?
Equipment affects inspection by controlling variables such as heat input, arc stability, gas shielding, joint alignment, cleanliness, and thermal history. If these variables are unstable, welds are more likely to show visual defects, lack of fusion, porosity, cracking, undercut, or unacceptable test results. Inspection success begins with equipment and procedure control before welding starts.