Spot welding equipment selection for sheet metal production
What spot welding equipment must control
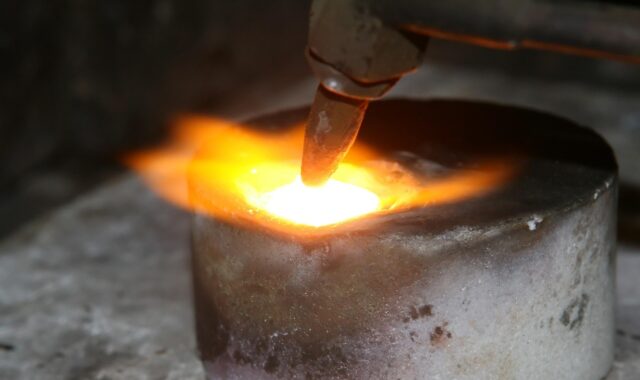
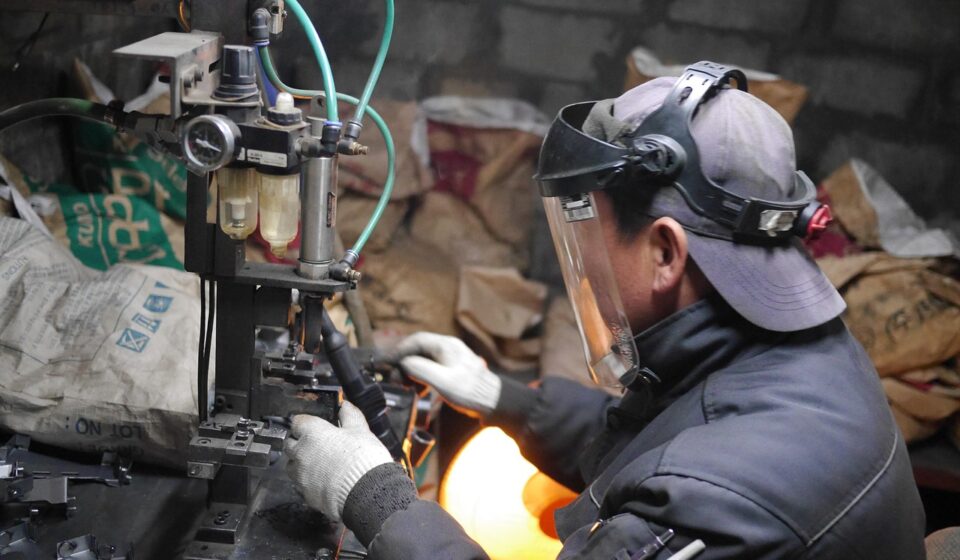
Spot welding equipment joins overlapping metal sheets by clamping them between electrodes, applying high current for a short time, and maintaining force while the weld nugget solidifies. For production teams, the selection question is not only machine size or purchase price. The equipment must repeat the required current, electrode force, weld time, cooling, alignment, and safety functions for the actual material stack-up. A small manual unit may produce acceptable trial welds, but coated steel, stainless steel, aluminum, battery tabs, or high-volume parts for process equipment can quickly expose limits in power capacity, rigidity, controls, and electrode life.
In a process equipment environment, spot welding may be used for sheet-metal housings, control cabinets, guards, ducting, trays, small brackets, filters, and light fabricated assemblies. The process is fast, normally does not require filler metal, and can be automated. Consistent results, however, depend on a balanced welding schedule. Heat input is often summarized as Q = I²Rt, where current, resistance, and time interact. In real production, electrode force, tip geometry, surface coating, cooling, and part fit-up strongly affect that equation.
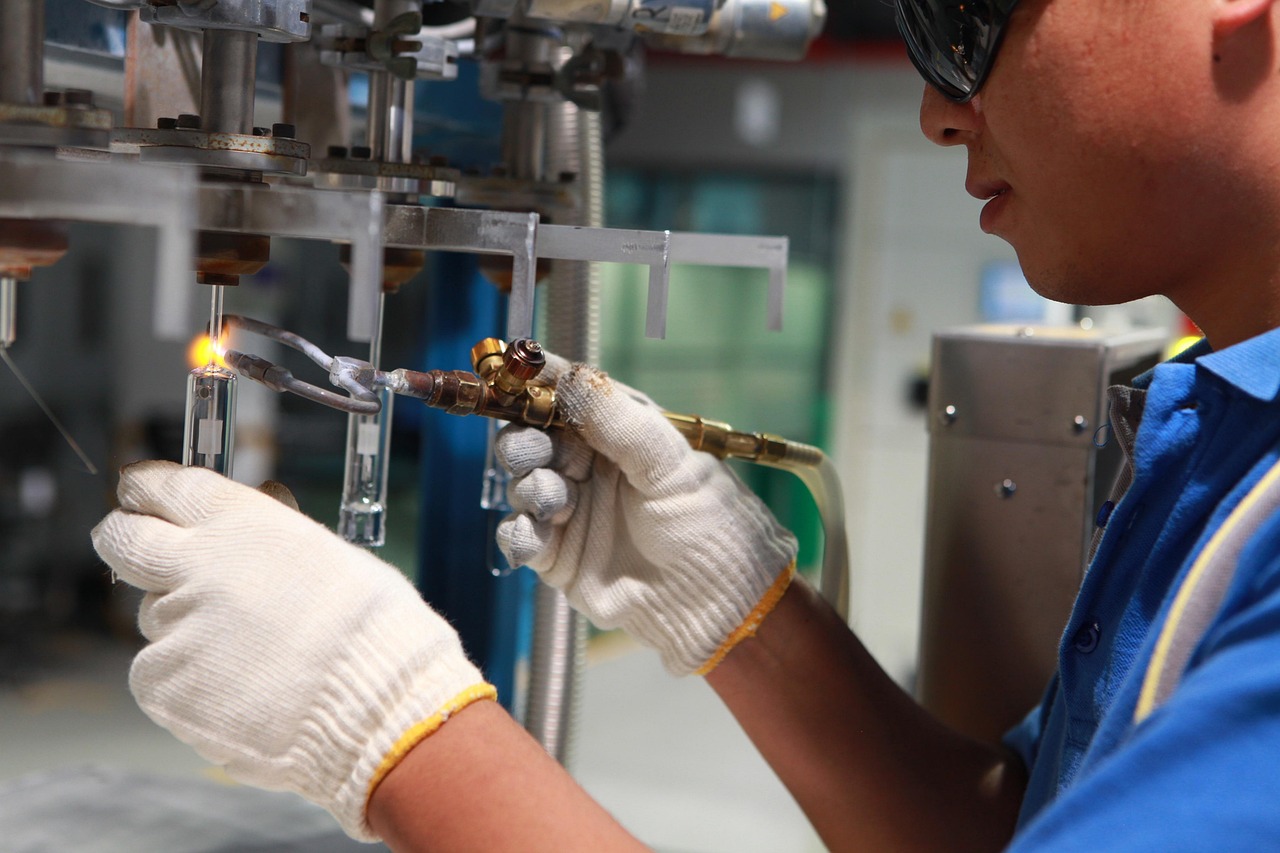
Main types of spot welding equipment
Different machine formats solve different production problems. The right choice depends on part size, joint access, cycle time, material thickness, and whether the operation is manual, semi-automatic, or robotic.
| Equipment type | Typical use | Selection notes |
|---|---|---|
| Bench or rocker-arm spot welder | Small sheet-metal parts, brackets, prototypes, repair work | Simple and compact in many cases, but throat depth, arm deflection, and operator consistency can limit repeatability. |
| Press-type spot or projection welder | Repeatable production welds, nuts, studs, projections, small assemblies | Provides better force control and easier fixture integration. Often preferred where weld location and force repeatability are critical. |
| Portable spot welding gun | Large assemblies that cannot easily be brought to a fixed machine | Requires attention to counterbalance, cable losses, operator ergonomics, and access to both sides of the joint. |
| Robotic C-gun or X-gun | Automotive-style body assemblies and high-volume cells | Combines programmed motion with weld schedule control. Requires careful fixture design, tip maintenance, and monitoring. |
| Capacitor-discharge or micro spot welder | Thin foils, small tabs, electronics, battery-related joining | Useful where short, controlled pulses are needed, but process qualification is material-specific. |
ISO 669:2016 identifies mechanical and electrical characteristics for resistance welding equipment and covers resistance spot, projection, seam, upset, and flash welding equipment. Its scope also recognizes several power source categories, including single-phase alternating current, rectified systems, and inverter transformer arrangements. This matters when comparing quotations because two machines with similar external dimensions may perform very differently under load.
Match the machine to the material stack
A common selection mistake is treating all sheet metal as one category. Spot welding equipment should be specified around the actual stack: material grade, coating, total thickness, number of layers, surface condition, flange width, access angle, and required weld spacing.
Low-carbon steel and stainless steel
Low-carbon steel is generally one of the more practical materials for resistance spot welding because it generates heat at the joint without requiring unusually high current. Stainless steels are also frequently spot welded, but they require attention to surface condition, distortion, marking, and corrosion expectations after welding. For cabinets, guards, and process equipment covers, the required cosmetic finish can be as important as weld strength.
Galvanized and other coated steels
Coated steels change the process window. Technical guidance from TWI notes that zinc-coated steels typically require higher welding current and higher electrode force than comparable uncoated steel, while the coating can alloy with copper electrode tips and shorten electrode life. This does not mean galvanized steel is unsuitable for spot welding. It means the equipment should have enough force, current capacity, cooling, and control range so the process is not run at the edge of the machine capability.
For production planning, electrode dressing and cap replacement should be treated as part of the process, not as occasional maintenance. If weld quality declines as tips mushroom or pick up coating, the cause may involve equipment capacity, cooling, tip material, or schedule control rather than operator error alone.
Aluminum, copper, and battery tabs
Aluminum and copper alloys are more demanding because their electrical and thermal behavior can move heat away from the weld zone. Aluminum often requires much higher current than steel of similar thickness. Copper can be difficult to weld with conventional copper alloy electrodes because the electrodes and workpiece have similar heat-generation behavior. For battery tabs, nickel strip, nickel-plated steel, copper, and aluminum combinations should not be assumed interchangeable. Small changes in coating, thickness, or tab geometry can require a new welding schedule and validation method.
Power source, controls, cooling, and mechanics
A useful equipment specification should cover more than nominal kVA. Buyers should ask how the machine controls secondary current, how force is generated and verified, how weld schedules are stored, and how the equipment responds to voltage variation, cable length, electrode wear, and cooling-water restrictions.
- Power source: Traditional AC equipment may be adequate for many steel applications. Medium-frequency DC systems can improve control and transformer packaging in automated cells. Capacitor-discharge systems are more common in small, high-energy pulse applications.
- Force system: Pneumatic systems are common, but servo force control can be useful where multiple materials, step schedules, or delicate components are involved.
- Mechanical rigidity: Arm deflection, gun stiffness, and fixture movement affect electrode alignment and real force at the weld. A machine that looks powerful on paper can still produce inconsistent welds if the frame flexes under load.
- Cooling: Water cooling protects electrodes, holders, transformers, and cables. Poor cooling accelerates tip wear and can narrow the welding window, especially on coated steels.
- Controls and monitoring: Modern controllers may store recipes, count welds, step current as electrodes wear, monitor current and voltage, and flag abnormal welds. Monitoring does not replace destructive validation, but it helps detect drift earlier.
For repeatable production, ask suppliers for data at the secondary side of the weld circuit, not only line-side ratings. Cable length, transformer placement, arm geometry, and gun type can all change the current available at the electrodes.
Standards and references that affect equipment choices
Standards do not select a machine automatically, but they help define what should be verified. The following references are especially relevant when preparing a purchase specification or internal validation plan.
| Reference | Date or edition | Why it matters for spot welding equipment |
|---|---|---|
| ISO 669 | 2016 edition, confirmed by ISO review in 2021 | Defines mechanical and electrical characteristics and test methods for resistance welding equipment specifications. |
| ISO 5821 | 2025 edition | Specifies dimensions and tolerances for female electrode caps used in resistance spot welding of metallic materials. |
| AWS C1.4M/C1.4 | 2025 edition | Provides requirements related to shear strength and weld button diameter for carbon and low-alloy steel sheet resistance and projection welds. |
| AWS C1.1M/C1.1 | 2019 edition with amendment information available from AWS | Provides recommended practices for resistance welding and is often used as a technical reference for schedules and procedure development. |
| OSHA 29 CFR 1910.255 | U.S. general industry rule for resistance welding | Covers installation, disconnecting means, operator instruction, guarding, shields, foot switches, emergency stops, grounding, and portable welding gun safety requirements. |
These references are not substitutes for project drawings, customer specifications, or local regulations. They do show why equipment selection should include documentation, inspection access, and operator safety from the beginning.
Quality control and maintenance requirements
Spot weld quality is often judged by weld nugget size, button diameter after destructive testing, peel or chisel test behavior, tensile shear performance, visual condition, and absence of excessive expulsion or indentation. The right acceptance method depends on the part, material, industry, and applicable standard. For critical assemblies, a validated weld schedule should be locked and checked periodically rather than adjusted informally on the shop floor. See also: Storage Systems.
Common causes of inconsistent welds include worn electrode tips, poor alignment, insufficient squeeze time, surface contamination, shunting through nearby welds, loose tooling, variable air pressure, poor cooling, and inadequate part fit-up. A good maintenance plan should include electrode dressing intervals, cap replacement rules, water-flow checks, cable inspection, force verification, current verification, and fixture condition checks.
For automated cells, weld counters and current stepping can help compensate for predictable electrode wear. The stepping interval and amount should be validated by testing because coating type, tip material, cooling, and part geometry all affect wear rate. For manual machines, written setup sheets and go/no-go checks are especially important because operator technique can change electrode placement and effective force.
Safety and compliance points to check before purchase
Resistance welding uses high current, moving clamps, hot metal, and possible flying sparks. In the United States, OSHA 29 CFR 1910.255 requires resistance welding equipment to be installed by a qualified electrician and to have a safety-type disconnecting switch, circuit breaker, or circuit interrupter located at or near the machine so power can be shut off for service. The same rule addresses operator instruction, guarding of automatic or air and hydraulic clamps, low-voltage external weld initiation circuits on nonportable spot and seam machines, interlocked access panels, point-of-operation guarding, spark shields, guarded foot switches, emergency stop buttons on special multispot machines, and counterbalance or support requirements for portable welding guns.
For buyers, safety should not be postponed until after commissioning. Ask whether the quoted machine includes guarding, emergency stops, shield provisions, interlocked cabinets, lockout points, clear electrical documentation, and maintenance access. Also confirm whether the supplier, integrator, or end user is responsible for risk assessment, guarding integration, and operator training.
A practical checklist for selecting spot welding equipment
- Define every material stack, including coatings, thickness range, number of layers, and surface finish expectations.
- Identify weld access, throat depth, flange width, weld spacing, and whether shunting from nearby welds may occur.
- Request secondary current capability, electrode force range, duty cycle, cooling requirements, and control features.
- Confirm whether the machine can store and protect weld schedules for different parts or materials.
- Specify electrode cap style, holder geometry, cooling path, and dressing or replacement method.
- Plan fixtures so they locate parts without stealing current from the weld path or forcing poor electrode alignment.
- Define acceptance criteria before buying equipment, not after the first production problem.
- Check applicable ISO, AWS, customer, and local safety requirements for the intended market.
- Include spare electrodes, caps, cables, transformers, sensors, and dressing tools in the lifecycle cost estimate.
- Run production-like trials using real parts, coatings, operators, and cycle times before final approval.
A sound purchase decision is usually based on a weld study rather than a catalog comparison. If a supplier can demonstrate stable welds on the real part, with documented schedules and destructive test evidence, the project risk is lower than relying on a generic power rating alone.
Frequently asked questions
Is spot welding equipment suitable for stainless steel process equipment parts?
It can be suitable for thin stainless sheet components such as covers, guards, light brackets, and enclosures. The decision should consider strength, appearance, corrosion expectations, access, and post-weld cleaning requirements. For pressure-retaining or code-governed parts, the applicable fabrication code and customer specification should control the joining method.
What is more important, welding current or electrode force?
Neither should be selected in isolation. Current creates heat, force controls contact and containment, and time determines how long heat is applied. Tip geometry, material resistance, surface coating, and cooling also affect the result. A stable weld schedule balances all of these variables.
Why do good spot welds become inconsistent during a shift?
Common reasons include electrode wear, coating buildup on the cap, reduced cooling, fixture looseness, material variation, air-pressure changes, and accumulated heat in the machine. A weld counter, electrode dressing schedule, and periodic force and current checks can reduce this drift.
Can one spot welder handle steel, aluminum, and copper tabs?
Sometimes, but it should not be assumed. These materials have different electrical resistance and thermal conductivity, and they may require different electrodes, current ranges, pulse profiles, and quality tests. Production trials on the real material stack are essential.
Should monitoring replace destructive weld testing?
No. Monitoring helps detect process drift, missing current, abnormal resistance, and some setup problems, but it should be tied to validated destructive or mechanical tests. The monitoring limits should be based on proven weld schedules, not arbitrary alarms.