How to specify stainless steel pumps and valves for chemical process lines
Selection starts with the process service
Stainless steel pumps and valves are widely specified for chemical process lines because they offer corrosion resistance, mechanical strength, cleanability and broad availability. The key point is that “stainless steel” is not one material choice. A pump casing, impeller, valve body, stem, ball, disc, seat, gasket and mechanical seal may each face different stresses, velocities and chemical exposure.
A sound specification starts with the service conditions: fluid composition, concentration, temperature, pressure, solids, viscosity, cleaning method, exposure time and the consequence of failure. In many projects, 316 or 316L stainless steel is a sensible baseline, but it is not a universal answer. Chlorides, strong acids, reducing conditions, abrasive slurries and crevice-prone designs can still cause rapid damage if the alloy, seal materials and surface condition are not matched to the duty.
For related equipment topics, readers can browse the Pumps and Valves section on Aizhika.
Why stainless steel is used in pumps and valves
Stainless steel is selected mainly because chromium in the alloy helps form a passive surface film that resists many forms of corrosion. In chemical equipment, that passive behavior can reduce rust contamination, improve washdown performance and extend service life compared with plain carbon steel in suitable environments. The benefit is most visible in wetted pump parts and valve internals, where corrosion products can damage seals, reduce flow area, contaminate product or prevent tight shutoff.
Stainless steel is corrosion-resistant, not corrosion-proof. The passive film can be damaged by low-oxygen crevices, high chloride concentration, high temperature, deposits, poor welding practice or aggressive cleaning chemicals. A line handling cool water with low chloride content may perform well with a standard austenitic stainless steel. A hot brine, hydrochloric acid stream or stagnant chloride solution may require duplex stainless steel, a nickel alloy, titanium, plastic-lined components or a nonmetallic design.
The specification should also distinguish between “stainless steel fitted” and “all stainless steel” equipment. A stainless-fitted pump may use stainless steel for selected wetted components while retaining other parts in iron or steel. An all-stainless wetted construction is different and should be defined by component, not assumed from a short catalogue description.
Match the alloy to the fluid, not only to the equipment name
304 and 304L stainless steel
304 stainless steel is widely used for water, mild chemicals, general washdown areas and many non-severe process services. It is available and cost-effective, but chloride resistance is its main limitation. Where chlorides, oxidizing salts, stagnant liquid or repeated wet-dry cycling are present, 304 can be vulnerable to pitting and crevice corrosion. 304L, the low-carbon version, is often preferred where welding is involved because it reduces the risk of sensitization in the heat-affected zone.
316 and 316L stainless steel
316 stainless steel contains molybdenum, which improves resistance to pitting and crevice corrosion compared with 304 in many chloride-bearing environments. Nickel Institute material guidance commonly identifies 316 as more resistant than 304 in chloride service, while still emphasizing that actual service limits depend on concentration, temperature, aeration and surface condition. 316L is frequently specified for welded wetted parts because its lower carbon content helps protect corrosion resistance after fabrication.
For chemical process pumps and valves, 316L is often used as a practical starting point for wetted castings, machined parts and sanitary components. It should not, however, be written as a blanket requirement without checking the chemistry. Strong hydrochloric acid, ferric chloride, hot seawater, hypochlorite solutions and other aggressive services may exceed the practical range of 316L.
Duplex, super duplex and higher alloys
Duplex stainless steels offer higher strength and better chloride stress-corrosion resistance than common 300-series austenitic stainless steels in many applications. They can be useful for brines, offshore utilities, certain wastewater duties and higher-pressure systems. Super duplex grades extend chloride resistance further, but they require careful welding control, procurement discipline and compatibility checks for cast parts, fasteners and seal chambers.
When stainless steel is marginal, the correct choice may be a higher nickel alloy, Alloy 20, titanium, zirconium, fluoropolymer lining or a nonmetallic pump. The selection should come from a corrosion review, not from the assumption that a more expensive stainless grade is automatically safer.
What to include in a stainless steel pump specification
A pump specification should begin with hydraulic and process data. Flow rate, differential head, suction pressure, net positive suction head available, liquid density, viscosity, vapor pressure, temperature range and solids content determine the pump type and operating margin. Material selection comes next, but it depends on the same data. A stainless steel centrifugal pump, rotary lobe pump, diaphragm pump or gear pump may all be correct in different services.
- Define every wetted component. List the casing, cover, impeller, shaft sleeve, seal chamber, wear rings, wetted fasteners and drain plugs. If cast stainless steel is used, state the cast grade or equivalent rather than only the wrought grade.
- Specify the seal system. Mechanical seal faces, springs, elastomers and flush plans must match the fluid. A stainless casing will not prevent failure if the elastomer swells, the seal faces abrade or solids clog the seal chamber.
- Consider crevices and drainage. Dead legs, unvented pockets and stagnant areas can become corrosion initiation points, especially with chlorides or cleaning chemicals.
- State surface finish where cleaning matters. Food, beverage, pharmaceutical and high-purity chemical lines may require polished surfaces, electropolishing, documented roughness values and clean-in-place capability.
- Request passivation where appropriate. ASTM A967/A967M-25 covers chemical passivation treatments for stainless steel parts, while ASTM A380/A380M is commonly referenced for cleaning, descaling and passivation practices. These documents do not prove that a grade is suitable for a chemical service; they help verify surface preparation.
For industrial centrifugal pumps, ISO 5199 is often used for Class II pump technical specifications, while API 610 is used for centrifugal pumps in petroleum, petrochemical and natural gas industry services. These standards address equipment design expectations; they do not replace a corrosion assessment for the actual fluid.
What to include in a stainless steel valve specification
Valve selection is often more complex than body material selection. A stainless steel valve body may be paired with a different stem, ball, disc, seat, packing, gasket or coating. The valve may also face local velocity, throttling erosion, pressure drop, cavitation or frequent cycling that the pipe and pump do not experience in the same way. See also: Storage Systems.
Valve type and function
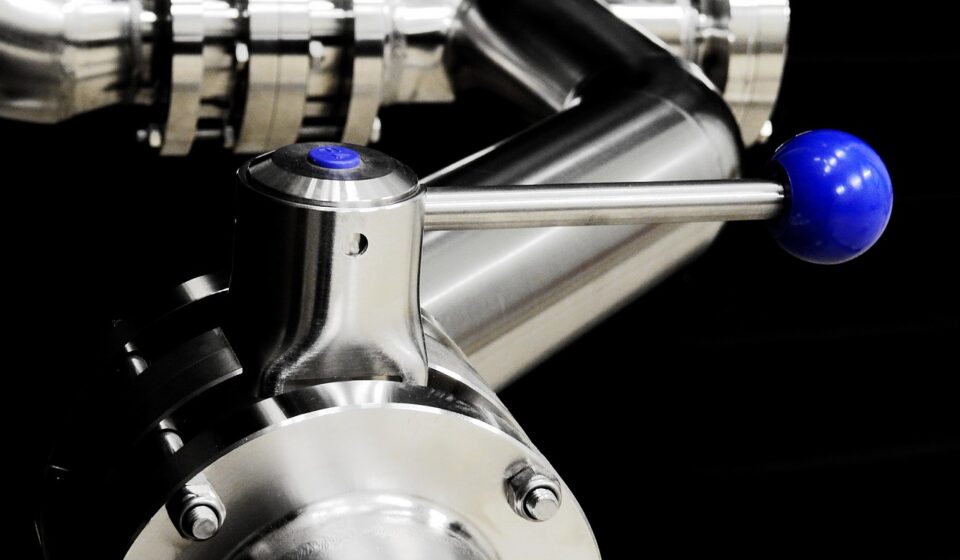
Ball valves are common for isolation and low-pressure-drop service. Butterfly valves are compact and frequently used in water, utility and hygienic services. Globe valves and characterized control valves are used where throttling accuracy matters. Diaphragm valves can isolate the process from the bonnet and are common in hygienic and corrosive services. Check valves require special attention because low flow, solids or pulsation can cause chatter and seat wear.
Pressure, temperature and leakage requirements
ASME B16.34-2025 covers pressure-temperature ratings, dimensions, materials, nondestructive examination, testing and marking for many steel, nickel-base and alloy valves. It is a useful reference for pressure boundary expectations, but it does not mean a soft seat, gasket or actuator is suitable at every listed body rating. Soft seats such as PTFE, reinforced PTFE, PEEK or elastomers have their own temperature and chemical limits. For production pressure testing, MSS SP-61-2019 establishes requirements and acceptance criteria for valve shell and seat closure pressure testing.
Trim, packing and actuation
The trim material should be specified separately from the body. Stainless stems and threaded parts can gall if materials, lubrication and hardness differences are not considered. Packing must resist the chemical and temperature while meeting fugitive emission or cleanliness requirements where they apply. Actuators should be selected for the required torque at the worst pressure differential, not only for the clean, new valve condition shown in a catalogue.
Standards and documents worth checking
Standards are most useful when they are tied to a specific design question. The table below summarizes common references that may appear in stainless steel pump and valve specifications. Project teams should verify the applicable edition, jurisdiction and contract requirement before purchase.
| Specification area | Common reference | What it helps verify |
|---|---|---|
| Chemical centrifugal pumps | ISO 5199 | Technical requirements for Class II centrifugal pumps, including design and operating expectations. |
| Petroleum and petrochemical pumps | API 610 | Requirements for centrifugal pumps in petroleum, petrochemical and natural gas industry process services. |
| Valve pressure boundary | ASME B16.34-2025 | Pressure-temperature ratings, materials, testing, marking and related requirements for many industrial valves. |
| Valve pressure testing | MSS SP-61-2019 | Shell and seat closure pressure testing requirements and acceptance criteria. |
| Passivation | ASTM A967/A967M-25 | Chemical passivation treatments and confirmation tests for stainless steel parts. |
| Pitting and crevice comparison | ASTM G48-25 | Laboratory methods for comparing resistance of stainless steels and related alloys in ferric chloride conditions. |
| Hygienic and high-purity service | ASME BPE-2024, 3-A Sanitary Standards, EHEDG guidelines | Design, cleanability, surface finish and hygienic construction expectations for bioprocessing, food and similar duties. |
| Drinking water contact | NSF/ANSI/CAN 61 | Health-effects requirements for products, components and materials in contact with drinking water. |
A standard reference should not be used as decoration. If the process requires NSF/ANSI/CAN 61 certification, for example, the finished component and its wetted materials should be certified for the intended contact conditions. If hygienic design is required, the specification should address cleanability, drainability, surface finish, elastomer compliance and documentation rather than simply asking for “sanitary stainless steel.”
A practical checklist before purchase
- Confirm the actual fluid. Include normal, startup, shutdown, cleaning and upset conditions. Small amounts of chloride, acid, oxidizer or solids can change the material decision.
- Set design limits. Define minimum and maximum temperature, pressure, flow, viscosity, vapor pressure and solids loading.
- Identify all wetted materials. Do not stop at the pump casing or valve body. Check trim, shaft sleeve, springs, fasteners, seats, gaskets and seal faces.
- Review corrosion mechanisms. Consider pitting, crevice corrosion, stress-corrosion cracking, erosion-corrosion, galvanic effects and contamination from fabrication.
- Define cleaning and surface requirements. CIP, SIP, passivation, electropolishing, roughness limits and drainability should be specified where they matter.
- Request documentation. Typical documents include material test reports, pressure test certificates, passivation records, surface finish records, dimensional drawings and conformity statements for named standards.
- Check maintenance access. A corrosion-resistant component still needs to be maintainable. Seal replacement, valve packing adjustment, seat inspection and cleaning access should be practical.
The best specification is specific enough to prevent substitution risk but not so narrow that it excludes technically acceptable alternatives. For example, it may be better to state the required corrosion resistance, wetted material grade, seal compatibility, test documentation and standard compliance than to copy a generic catalogue code.
Frequently asked questions
Are 316 stainless steel pumps and valves always better than 304?
No. 316 is usually more resistant than 304 to chloride-related pitting because of its molybdenum content, but “better” depends on the fluid, temperature, cleaning chemicals, availability and cost. In low-chloride, mild services, 304 may be adequate. In severe chloride or acid service, 316 may still be inadequate.
When should 316L be specified instead of 316?
316L is commonly preferred for welded wetted parts, hygienic systems and equipment that will be passivated or polished after fabrication. The lower carbon content helps reduce sensitization risk near welds. It does not make the alloy immune to chloride attack or strong acid corrosion.
Can stainless steel pumps handle hydrochloric acid?
Common austenitic stainless steels are often poor choices for hydrochloric acid, especially as concentration or temperature increases. Some dilute, controlled conditions may be possible, but this service usually requires a specific corrosion review and may point toward lined equipment, high-nickel alloys or nonmetallic materials.
What documents should be requested with stainless steel valves?
Useful documents include material test reports for pressure-containing and wetted parts, pressure test records, seat test records, packing and gasket material data, valve drawings, marking details and any certificates required by the project standard. For hygienic or drinking-water service, certification should apply to the relevant finished product and use condition.
Does passivation replace good material selection?
No. Passivation improves the cleanliness and passive condition of a suitable stainless surface, but it cannot make the wrong alloy suitable for a corrosive chemical. It should be treated as a fabrication and quality step, not as a substitute for compatibility analysis.