How to seal pumps and valves in chemical service
Why sealing choices matter in pumps and valves
To seal pumps and valves in chemical service, engineers need to treat pump shaft sealing and valve stem sealing as related but separate reliability problems. Pumps most often leak at the rotating shaft seal. Valves more commonly leak at the stem, gland, body joints, or seat. The suitable choice depends on the fluid hazard, vapor pressure, temperature, pressure cycling, shaft speed, valve motion, maintenance access, and the site’s leak detection obligations.
For hazardous, flammable, odorous, toxic, or volatile fluids, the decision is rarely just “packing or mechanical seal.” It becomes a specification process that connects equipment design, seal support systems, packing qualification, installation discipline, and monitoring.
In chemical plants, seals are small components with large consequences. A poor sealing decision can increase fugitive emissions, contaminate product, expose maintenance teams to hazardous fluids, shorten bearing life, or force an unplanned shutdown. The useful question is not which seal is universally best, but which sealing arrangement fits the fluid, duty cycle, environmental limits, and maintenance strategy.
This article summarizes the main decisions behind pump and valve sealing for chemical equipment readers. For related fluid-handling topics, see the Pumps and Valves section.
Pump seals and valve seals solve different problems
Pumps and valves both contain process fluid, but their sealing interfaces work in different ways. A centrifugal or rotary pump has a rotating shaft passing through a pressure boundary. The seal must control leakage while allowing rotation, removing heat, tolerating vibration, and surviving transient operating conditions.
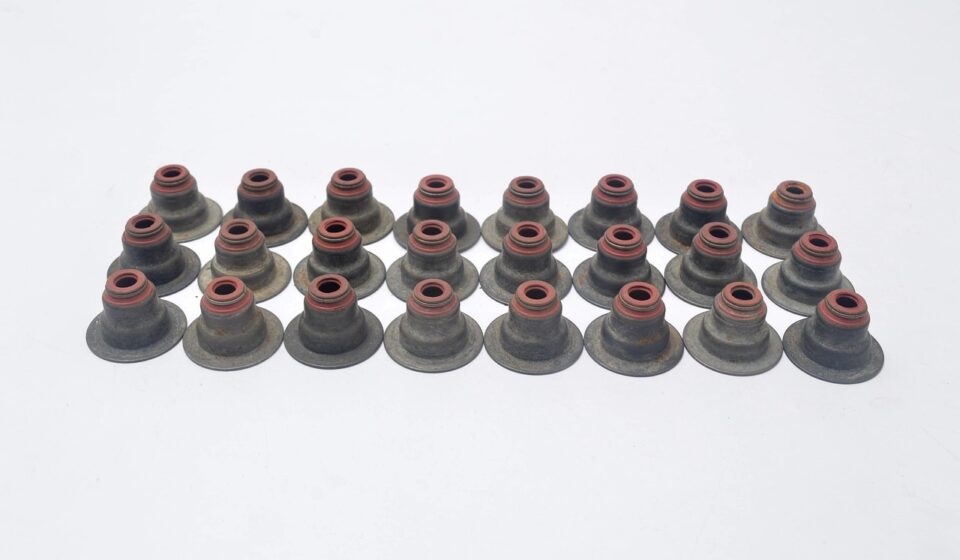
A valve often has a rising, rotating, or quarter-turn stem. Its packing must seal around movement that may be intermittent rather than continuous. The valve seat also has a separate job: providing internal shutoff when the valve is closed.
This difference explains why pump specifications usually focus on mechanical seal arrangement, seal chamber conditions, flush plans, barrier or buffer fluids, and dry-running risk. Valve specifications focus more on stem packing material, gland loading, emissions qualification, seat leakage class, fire-safe requirements where relevant, and whether the valve design can be adjusted or repaired in service.
Environmental guidance from the U.S. Environmental Protection Agency identifies pumps, valves, connectors, pressure relief devices, and similar components as common sources of equipment leaks in refineries and chemical manufacturing. The EPA’s LDAR best-practice material also notes a practical distinction: pump leaks typically occur at the seal, while valve leaks often occur at the stem or gland area because of packing or O-ring problems. That leak-location map is useful when planning inspections and spare parts.
Main pump sealing options
Packed glands
Packed glands use rings of packing compressed in a stuffing box around the shaft. They are familiar, relatively simple, and can be practical for some water, slurry, utility, and non-hazardous duties. Their limitation is that they normally require controlled leakage for lubrication and cooling. If the gland is tightened too much, the packing can overheat, score the shaft sleeve, and fail. If it is too loose, leakage becomes unacceptable.
For chemical service, packed glands need careful review. They may be unsuitable where leakage of volatile, toxic, flammable, corrosive, or valuable fluids cannot be tolerated. They also require maintenance discipline because packing adjustment is a wear-management activity, not a one-time installation task.
Single mechanical seals
A single mechanical seal uses rotating and stationary faces, secondary seals, springs or bellows, and a gland arrangement to limit leakage at the shaft. It usually provides better containment than compression packing, but it still depends on a stable fluid film between the seal faces. Heat, solids, vaporization, dry running, misalignment, and pressure upsets can quickly reduce seal life.
Single seals are often considered for clean, compatible liquids where small controlled leakage or vapor emission is acceptable under the site’s safety and environmental rules. They become risky when the fluid is prone to crystallization, polymerization, flashing, coking, or abrasive wear unless the seal environment is properly engineered.
Dual mechanical seals
Dual seals add a second sealing interface and use buffer or barrier fluid between the seals. An unpressurized dual seal can help contain leakage and route it to a safe collection system. A pressurized dual seal uses barrier fluid at a pressure above the process side so that leakage direction is controlled toward the process rather than outward to atmosphere. This can be important for toxic, hazardous, high-vapor-pressure, or environmentally sensitive services.
The trade-off is complexity. Dual seals require support systems, level or pressure monitoring, heat removal, proper commissioning, and maintenance of the barrier or buffer fluid. A dual seal without a maintained support system can become less reliable than a simpler arrangement that is correctly applied.
Sealless pumps
Magnetic-drive and canned-motor pumps remove the dynamic shaft penetration through the casing. They can be attractive for highly hazardous, odorous, expensive, or difficult-to-contain liquids. However, sealless does not mean maintenance-free. The containment shell, bearings, heat generation, dry-running protection, solids tolerance, and secondary containment philosophy all need review. For some slurries, crystallizing liquids, or services with frequent off-design operation, a robust sealed pump may still be more practical.
Seal plans are part of the pump seal, not an accessory
A mechanical seal rarely succeeds on hardware alone. Seal faces need adequate lubrication, cooling, cleanliness, and pressure control. That is why pump specifications often include a seal piping or flush plan. API Standard 682, widely used in petroleum, natural gas, and chemical pump services, defines shaft sealing systems for centrifugal and rotary pumps and organizes seals by categories, types, arrangements, and orientations. API’s published description of the fourth edition states that it applies mainly to hazardous, flammable, or toxic services where improved equipment availability, reduced atmospheric emissions, and lower life-cycle sealing costs are important.
Common seal-plan functions include routing clean process liquid to the seal chamber, removing heat, separating solids, maintaining barrier-fluid pressure, detecting leakage, and providing safe venting or draining. Hydraulic Institute training materials and pump-industry guidance emphasize that seal piping plans depend on correct tubing layout, elevation, pressure settings, instrumentation, cleanliness, and commissioning checks.
| Seal plan function | Why it matters | Typical risk if ignored |
|---|---|---|
| Flush and circulation | Provides cooling and lubrication at seal faces | Face overheating, flashing, or early wear |
| Solids control | Reduces abrasive particles at the seal interface | Grooved faces, leakage, sleeve damage |
| Barrier or buffer fluid | Controls leakage direction and collects emissions | Loss of containment or undetected seal failure |
| Instrumentation | Shows pressure, level, temperature, or flow problems | Operation continues after the support system has failed |
| Venting and draining | Removes trapped gas and permits safe maintenance | Dry running, unsafe opening, or poor startup reliability |
A common pump-seal mistake is specifying a recognized seal arrangement while treating the support plan as secondary. In practice, seal plan details often determine whether the selected seal survives the actual chemical service.
Valve sealing focuses on packing, stem motion, and emissions qualification
Valve sealing has two separate questions. First, can the valve prevent external leakage around the stem, bonnet, body joints, and other pressure-boundary interfaces? Second, can it control internal leakage across the seat when closed? For fugitive emissions, the stem packing system receives the most attention because it must maintain tightness while allowing movement. See also: Storage Systems.
Flexible graphite packing is widely used in higher-temperature and chemical services, but material selection alone does not guarantee low leakage. Packing performance depends on stem finish, gland geometry, live loading where used, bolt stress, corrosion, thermal cycling, pressure cycling, and the number of valve strokes. A valve installed in a vibrating line or operated frequently may challenge the packing differently from the same valve left mostly open or closed.
Several recognized standards help organize valve-emissions expectations. API Standard 622 addresses type testing of process valve packing for fugitive emissions and considers factors such as temperature, pressure, thermal cycling, mechanical cycling, and corrosion. API Standard 624 applies to type testing of rising stem valves equipped with flexible graphite packing. API Standard 641 covers type testing of quarter-turn valves for fugitive emissions. ISO 15848-1 provides a classification and qualification framework for external leakage of valve stem or shaft seals and body joints in valves intended for volatile air pollutants and hazardous fluids.
These standards are not interchangeable labels. API 622 is about packing qualification, while API 624 and API 641 evaluate valve assemblies. ISO 15848 uses its own classification approach. A buyer should state the required standard, edition, leakage class where applicable, test medium expectations, temperature range, and documentation requirements rather than asking only for a “low-emission valve.”
How service conditions drive the specification
The right way to seal pumps and valves is to start with the service, not the catalog category. The following factors usually decide whether a simple arrangement is acceptable or a more engineered sealing system is needed.
- Fluid hazard: Toxic, carcinogenic, flammable, odorous, or environmentally restricted fluids usually justify tighter sealing and stronger monitoring.
- Vapor pressure and flashing risk: Liquids near their vapor-pressure limit can vaporize at seal faces, destroying lubrication and increasing leakage risk.
- Temperature: High temperature accelerates packing oxidation, elastomer aging, face distortion, and barrier-fluid degradation. Low temperature can affect elastomer flexibility and condensation behavior.
- Solids and crystallization: Slurries, salts, polymers, and crystallizing fluids may require flush control, hardened faces, special clearances, or a different pump type.
- Pressure cycling: Frequent startups, shutdowns, and batch operation can challenge both pump seals and valve packing more severely than steady operation.
- Maintenance access: A theoretically superior seal is not practical if the plant cannot inspect, refill, isolate, or safely repair the support system.
- Regulatory exposure: Facilities subject to LDAR rules may need component identification, monitoring intervals, repair records, and defined repair timelines.
In practice, chemical plants often over-focus on the sealing component and under-specify the operating envelope. A pump seal selected for normal flow and temperature may fail during blocked suction, hot standby, reverse rotation, or poor venting. A valve packing set qualified in a laboratory may perform poorly if installed on a damaged stem or loaded unevenly. The specification should therefore include the service envelope and the quality checks that keep the seal operating within that envelope.
Standards and guidance to reference in specifications
Standards do not replace engineering judgment, but they reduce ambiguity between plant owners, EPC contractors, distributors, and manufacturers. The most relevant documents for sealing pumps and valves in chemical service include the following.
| Document or guidance | Equipment focus | Practical use in a specification |
|---|---|---|
| API Standard 682 | Pump shaft sealing systems | Defines mechanical seal arrangements, categories, orientations, and support-system expectations for centrifugal and rotary pumps in demanding services |
| API Standard 622 | Process valve packing | Helps qualify packing for fugitive-emission performance under defined mechanical and thermal conditions |
| API Standard 624 | Rising stem valves | Applies emissions type testing to valve assemblies equipped with flexible graphite packing |
| API Standard 641 | Quarter-turn valves | Applies emissions type testing to quarter-turn valve assemblies |
| ISO 15848-1 | Industrial valve fugitive emissions | Classifies and qualifies external leakage performance for valve stem or shaft seals and body joints |
| EPA LDAR guidance | Leak monitoring and repair programs | Supports inspection planning for pumps, valves, connectors, and other components in regulated services |
When writing a purchase specification, avoid vague phrases such as “standard mechanical seal,” “chemical-duty packing,” or “emission-proof valve.” Better wording identifies the standard, edition if required by the project, operating case, materials, allowable leakage or emissions requirement, documentation, test certificates, and any site-specific maintenance constraints.
Installation and maintenance determine real leakage performance
Even a well-selected seal can fail early if installation is poor. For pumps, common problems include pipe strain, shaft runout, soft foot, coupling misalignment, clogged flush lines, incorrect orifice sizing, inadequate venting, contaminated barrier fluid, and startup before the seal chamber is fully flooded. For valves, frequent problems include scratched stems, uneven gland loading, over-compressed packing, insufficient retightening after thermal cycling, and actuator side loads.
A useful maintenance program separates visible leakage control from root-cause correction. Tightening a gland or topping up a barrier-fluid reservoir may stop the immediate symptom, but it does not explain why the leak started. Plants should track repeated failures by service, equipment tag, seal type, valve type, packing set, temperature, and operating mode. Patterns often show that the issue is not the seal brand but an unsuitable flush plan, vaporizing service, line vibration, poor installation practice, or a valve being used for throttling when it was selected mainly for isolation.
For LDAR-covered services, maintenance records also need to support compliance. Depending on the applicable regulation and component category, programs may include Method 21 monitoring, visual or audible checks, repair attempts within defined periods, delay-of-repair documentation, and verification after maintenance. Because legal obligations vary by jurisdiction, plant type, and service, project teams should confirm the governing rule before finalizing monitoring intervals or repair deadlines.
Specification checklist for chemical plant teams
- Define the fluid, concentration, vapor pressure, solids content, toxicity, flammability, odor threshold, and environmental limits.
- List normal, minimum, maximum, startup, shutdown, standby, cleaning, and upset conditions.
- For pumps, specify seal arrangement, materials, flush or barrier plan, instrumentation, venting, drain routing, and dry-running safeguards.
- For valves, specify packing qualification, valve emissions standard, stem finish, gland design, actuator loads, fire-safe needs where relevant, and seat leakage expectation.
- Confirm whether the component is part of an LDAR program and what monitoring method, tag records, and repair documentation are required.
- Require installation checks for alignment, pipe strain, torque, cleanliness, support-system pressure, and commissioning records.
- Keep spare parts consistent with the approved seal and packing bill of materials; uncontrolled substitutions can invalidate the original specification logic.
- Review failure history before repeating the same seal selection on similar services.
Frequently asked questions
Are mechanical seals always better than packing for pumps?
No. Mechanical seals usually provide better containment for many chemical services, especially where emissions or housekeeping matter. However, they are more sensitive to dry running, poor flush conditions, vibration, and installation errors. Packing can still be practical for selected non-hazardous or abrasive services if controlled leakage is acceptable and maintenance is planned.
What is the difference between pump sealing and valve sealing?
Pump sealing mainly controls leakage where a rotating shaft exits the casing. Valve sealing controls external leakage around the stem or body joints and internal leakage across the seat. Pump seals require attention to face lubrication and support plans, while valve seals require attention to packing load, stem movement, emissions qualification, and seat design.
When should a dual mechanical seal be considered?
A dual seal should be considered when the pumped liquid is toxic, flammable, volatile, odorous, environmentally sensitive, or likely to create unacceptable leakage risk with a single seal. It is also useful when leakage must be collected, diluted, monitored, or prevented from reaching atmosphere. The support system must be maintained for the dual seal to deliver its intended benefit.
Does a low-emission valve eliminate LDAR requirements?
Not necessarily. A low-emission valve can reduce leak probability and may support a plant’s emissions strategy, but monitoring and repair duties depend on the applicable regulation, permit, service classification, and facility program. Engineering specifications and compliance programs should be aligned before procurement.
What information should be given to a seal or valve supplier?
Provide the fluid composition, temperature and pressure range, vapor pressure, solids, corrosion data, operating cycle, equipment speed or valve motion, emissions requirement, applicable standards, installation constraints, and monitoring expectations. Complete service data is often more valuable than asking for a generic chemical-duty seal.