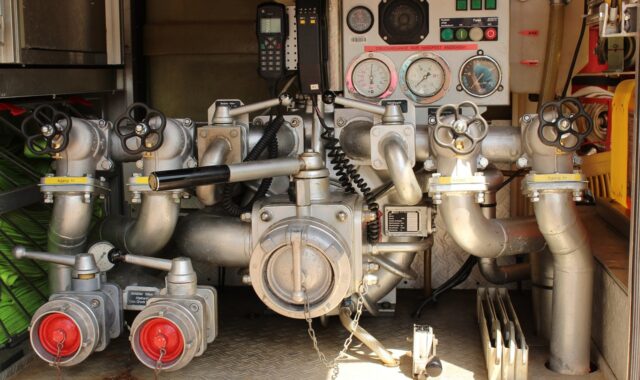
Hydraulic pump and valve selection for reliable industrial fluid power systems
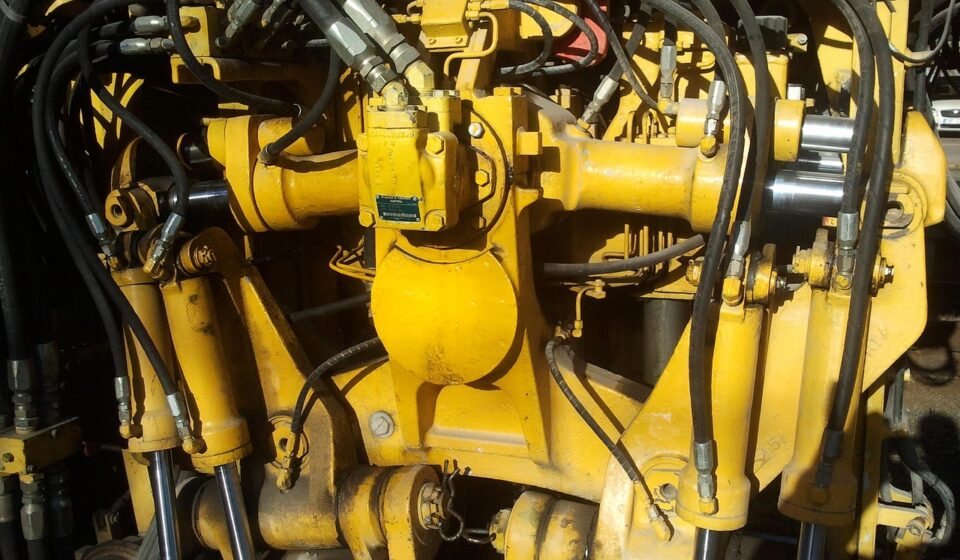
What a hydraulic pump and valve do in one circuit
A hydraulic pump and valve set performs reliably when it is selected as a matched control system, not as separate catalog items. The pump converts mechanical input from an electric motor or engine into hydraulic flow. Valves then control where that flow goes, how much pressure the circuit can build, how fast an actuator moves and how safely stored energy is released.
In industrial equipment, especially machinery operating near chemical processing areas, poor matching can lead to heat, pressure spikes, erratic motion, leakage, seal damage and avoidable downtime. The practical sequence is to define the required actuator force and speed first, then select the pump, valves, filtration and controls that can deliver those conditions within safe operating limits.
This guide focuses on functional selection rather than brand comparison. It refers to recognized industry sources such as ISO 4413 for hydraulic system safety, ISO 4406 for fluid cleanliness coding, ISO 1219-1 for hydraulic symbols, OSHA lockout/tagout requirements for hazardous energy control in the United States, and Hydraulic Institute and U.S. Department of Energy guidance on pumping system lifecycle thinking. For related industrial equipment topics, see the Pumps and Valves category.
Start with the duty, not the component list
The most common selection error is choosing a pump frame size or valve port size before the machine duty is clear. A hydraulic circuit should start with four operating questions: what load must be moved, how fast it must move, how often the cycle repeats and what environment the system will operate in. These answers drive pressure, flow, heat rejection, reservoir size, filtration level and valve response.
Pressure is related to force. Flow is related to actuator speed. Duty cycle affects temperature and component life. Environment affects material compatibility, enclosure rating, corrosion protection and maintenance access. A press that holds pressure for long periods has different requirements from a fast indexing machine, even if both use similar nominal pump flow. A mixer lift in a corrosive area has different seal and coating concerns from a clean indoor test bench.
Before specifying hardware, define the following baseline values:
- Maximum working pressure and expected pressure peaks.
- Required flow during extension, retraction, holding and idle conditions.
- Cycle frequency, operating hours and acceptable temperature rise.
- Fluid type, viscosity range and compatibility with seals, hoses and coatings.
- Cleanliness target, filtration plan and sampling method.
- Required manual override, emergency stop, isolation and maintenance functions.
Choose the pump by flow profile and control strategy
A pump does not create useful work by pressure alone. It supplies flow against system resistance, and pressure rises only as the load demands it. That distinction matters. An oversized pump can waste energy and generate heat, while an undersized pump can make actuators slow or unstable. The right pump type depends on the required flow profile, pressure range, noise limits, efficiency target and control method.
Fixed-displacement pumps
Gear, vane and fixed piston pumps deliver a set amount of fluid per shaft revolution. They are often selected for simplicity and predictable output. A fixed-displacement pump can be a good fit when the machine has steady demand, or when cost and ease of maintenance are priorities. However, if the pump continues to deliver high flow while the circuit is throttled or held at pressure, excess energy becomes heat. In that case, unloading valves, accumulator circuits, variable-speed drives or a different pump strategy may be needed.
Variable-displacement pumps
Variable-displacement piston pumps can adjust output according to pressure, flow or load-sensing control requirements. They can reduce wasted flow when demand changes during the machine cycle. They also add control settings and maintenance sensitivity, so the system needs proper filtration, stable pilot pressure and clear commissioning procedures. In applications with frequent idle time, changing loads or multiple actuators, variable-displacement control can reduce heat and improve responsiveness when correctly applied.
Pressure rating and margin
The pump rating should cover continuous working pressure and expected transient peaks, but excessive oversizing is not automatically safer. Oversized pumps may require larger valves, larger reservoirs, higher motor power and more cooling capacity. A better approach is to calculate the duty, review the relief setting, account for line losses and confirm that each component remains within the manufacturer’s specified limits during all operating modes.
Select valves by function, not by name alone
Hydraulic valve selection can be confusing because one manifold may combine pressure, directional, flow, check and proportional functions in a compact block. The valve name is less important than the function it performs in the circuit. A clear schematic, normally based on ISO 1219-1 symbols, helps engineering, purchasing and maintenance teams discuss the same function without relying on vague descriptions.
Pressure control valves
Relief valves protect circuits from overpressure by opening when pressure reaches a set level. Reducing valves maintain a lower pressure in a branch circuit. Sequence valves allow one operation to occur after another pressure condition is met. Counterbalance valves help control overrunning loads and prevent uncontrolled actuator movement. These valves should be set and tested under realistic load conditions, because bench settings may not reflect installed behavior.
Directional control valves
Directional valves route flow to extend, retract, stop or float an actuator. The spool configuration matters. A closed-center spool, open-center spool and tandem-center spool can produce very different idle pressure, heat generation and actuator holding behavior. Solenoid valves may be adequate for simple on-off motion, while hydraulically piloted or proportional directional valves may be needed for larger flows, smoother motion or remote control.
Flow control and proportional valves
Flow control valves regulate actuator speed by limiting or compensating flow. Simple throttle valves are inexpensive but can be sensitive to pressure changes. Pressure-compensated flow controls improve speed consistency when load varies. Proportional and servo valves provide finer control, but they require cleaner fluid, stable electronics and careful commissioning. In high-value equipment, the extra control may be justified; in a rugged utility circuit, a simpler valve may be more reliable.
Check compatibility across the whole hydraulic system
A pump and valve may each appear suitable on paper but fail as a pair if flow, pressure drop, pilot supply, response time or fluid compatibility is overlooked. The following table summarizes practical cross-checks before releasing a design or purchasing replacement parts.
| Selection check | Why it matters | What to verify |
|---|---|---|
| Pump flow versus valve capacity | Undersized valves add pressure drop and heat | Rated flow, acceptable pressure drop and port sizing |
| Relief setting versus component ratings | Weak components may see peak pressure | Lowest-rated hose, fitting, actuator, valve and manifold section |
| Pilot pressure availability | Piloted valves may not shift reliably without stable control pressure | Minimum pilot pressure during startup, idle and load changes |
| Fluid and seal compatibility | Chemical exposure and fluid type can shorten seal life | Elastomer material, hose liner, coating and fluid data |
| Cleanliness target | Contamination can damage pumps and precision valves | ISO 4406 cleanliness code target, filter rating and sampling point |
| Maintenance access | Hidden components increase troubleshooting time | Gauge ports, isolation valves, drain points and safe access space |
For chemical and process environments, compatibility deserves extra attention. Hydraulic oil may be exposed to moisture, washdown, airborne chemicals or elevated ambient temperature. The selected fluid must remain within viscosity limits at startup and at full operating temperature. Seals and hoses should be checked against both the hydraulic fluid and likely external exposure. Where fire risk is a concern, the fluid choice and component compatibility should be reviewed with the equipment manufacturer and relevant site safety standards.
Control heat, energy use and lifecycle cost
Heat is one of the clearest signs that the pump and valve strategy needs review. It usually comes from energy that enters the system but does not become useful actuator work. Common sources include excessive throttling, relief valves passing continuously, undersized lines, restrictive filters, unnecessary pressure drop through valves and pumps running at full flow during idle time.
Hydraulic Institute and U.S. Department of Energy pumping system guidance emphasizes lifecycle cost rather than purchase price alone. The same principle applies to hydraulic power units. A lower-cost pump may become expensive if it forces the system to run hotter, requires a larger cooler or causes frequent seal replacement. A more efficient control strategy may reduce operating cost, but it must still be maintainable by the site team. See also: Storage Systems.
Useful energy and heat checks include:
- Measure pressure before and after key valves to identify avoidable pressure drop.
- Confirm whether the relief valve is passing during normal operation.
- Compare actual actuator speed with calculated flow demand.
- Trend reservoir temperature during a full production cycle, not only at startup.
- Review whether idle periods justify pump unloading, variable displacement or variable motor speed.
Efficiency decisions should be made at system level. A highly efficient pump can still waste energy if the valves constantly throttle flow. A sophisticated valve can still perform poorly if the pump response is unstable. The best result usually comes from reducing unnecessary pressure drop, matching flow to demand and keeping fluid within the recommended viscosity and cleanliness range.
Build safety and maintainability into the design
Hydraulic systems can store hazardous energy in pressurized lines, accumulators, suspended loads and trapped fluid volumes. ISO 4413:2010, which ISO lists as confirmed in 2021, specifies general rules and safety requirements for hydraulic fluid power systems and their components on machinery. It addresses hazards, design, construction, modification, installation, maintenance, reliable operation, energy efficiency and environmental considerations. In U.S. workplaces, OSHA 29 CFR 1910.147 also requires control of hazardous energy during servicing and maintenance when the regulation applies.
Good hydraulic pump and valve design therefore includes more than rated pressure. It should provide safe isolation, controlled depressurization, clear labeling, accessible test points and documented settings. Accumulators require special attention because stored pressure may remain after the pump stops. Loads that can fall or overrun need appropriate holding and counterbalance functions, not only a directional valve in the neutral position.
Maintainability is also a safety issue. If technicians cannot read the schematic, reach the filter, connect a gauge or identify the correct valve cartridge, troubleshooting becomes slower and riskier. A practical hydraulic power unit should include a current schematic, component tags, pressure test points, filter indicators, drain access and enough space to replace wear parts without dismantling unrelated equipment.
Use commissioning data to prevent recurring failures
Commissioning should create a baseline for future troubleshooting. At minimum, record relief settings, standby pressure, working pressure under load, pump case drain flow where applicable, reservoir temperature, filter condition, actuator cycle time and fluid cleanliness. These values help separate a design issue from a maintenance issue later.
Recurring pump failure may point to cavitation, aeration, contamination, excessive case pressure or incorrect fluid viscosity. Recurring valve sticking may point to dirty fluid, varnish, damaged coils, unstable pilot pressure or incorrect spool selection. Slow actuator movement may be caused by pump wear, internal leakage, low relief setting, blocked filters, undersized valves or excessive load. Without baseline data, each symptom can lead to unnecessary part replacement.
A practical troubleshooting sequence is to verify the fluid first, then pressure, then flow, then valve command and actuator condition. Clean oil at the correct viscosity will not solve every problem, but dirty or unsuitable oil can undermine even a well-designed system. ISO 4406:2021 provides a standardized method for coding particle contamination levels in hydraulic fluid, making it easier to set cleanliness targets and compare oil analysis results.
Frequently asked questions
What is the difference between a hydraulic pump and a hydraulic valve?
A hydraulic pump supplies flow to the circuit by converting mechanical input into hydraulic energy. A hydraulic valve controls that flow by directing it, limiting pressure, regulating speed or holding a load. The pump provides the source of flow; the valve determines how the circuit uses it.
Can a larger hydraulic pump improve machine performance?
Not always. A larger pump may increase available flow, but it can also create more heat, require more motor power and overload valves or lines if the rest of the circuit is not sized for it. Performance should be improved by calculating actual force, speed and duty requirements before changing pump size.
Why does a hydraulic valve overheat?
A valve itself does not usually generate heat without a pressure drop and flow through it. Overheating can occur when flow is throttled continuously, a relief valve passes during normal operation, a valve is undersized or the control strategy forces the pump to produce more flow or pressure than the machine needs.
How important is oil cleanliness for pumps and valves?
Oil cleanliness is critical, especially for piston pumps, proportional valves and close-clearance components. Particle contamination can accelerate wear, cause sticking and reduce reliability. A defined ISO 4406 cleanliness target, suitable filtration and regular sampling are more reliable than visual oil checks alone.
What documents should be kept with a hydraulic system?
Keep the latest schematic, bill of materials, valve setting record, fluid specification, filter details, maintenance history, oil analysis results and commissioning baseline. These records reduce troubleshooting time and help ensure replacement parts match the original design intent.
Key takeaway
Reliable hydraulic pump and valve selection is a system decision. The pump must match the required flow and pressure profile, the valves must control that flow safely, the fluid must stay clean and compatible, and the design must allow safe maintenance. When these elements are reviewed together, industrial equipment is less likely to suffer from heat, unstable motion, premature wear and avoidable downtime.