Arc welding equipment explained for process equipment fabrication
What arc welding equipment includes
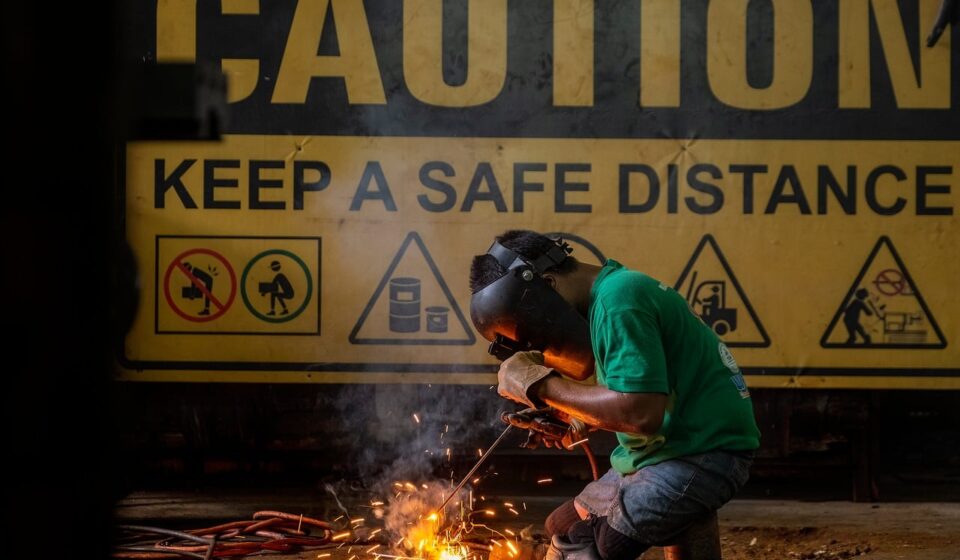
Arc welding equipment uses an electric arc to generate the heat needed to fuse metals. In fabrication and maintenance work, however, the equipment package is much broader than the welding machine. It normally includes the power source, torch or electrode holder, work clamp and return cable, welding leads, consumables, shielding gas system where required, controls, cooling accessories, fume control, and personal protective equipment.
For process equipment fabrication, repair, and maintenance, the right setup depends on the welding process, base material, joint access, code requirements, production volume, and working environment. Tanks, pressure-related assemblies, piping, support frames, platforms, skids, and plant repairs may all involve arc welding, but they do not all suit the same machine. A compact stick welding setup may be practical for field repair. Semiautomatic gas metal arc welding may be better for repeated shop welds. Gas tungsten arc welding may be selected where control and weld cleanliness are more important than travel speed.
For readers comparing fabrication and maintenance choices across industrial systems, the Process Equipment section provides related context on equipment used in chemical and process plants.
Main arc welding processes and how the equipment differs
The first selection step is to identify the welding process. Industry sources such as the American Welding Society commonly distinguish several widely used arc welding processes, including shielded metal arc welding, gas metal arc welding, gas tungsten arc welding, and flux-cored arc welding. Each process creates and controls the arc differently, so the equipment configuration also changes.
Shielded metal arc welding
Shielded metal arc welding, often called SMAW or stick welding, uses a flux-coated consumable electrode. The equipment is comparatively simple: a power source, electrode holder, work lead, cables, and electrodes. Because it does not need a separate shielding gas cylinder, SMAW is often useful for outdoor repair, maintenance, and jobs where portability matters. Its limitations include lower deposition rates than many wire-fed processes and the need to remove slag between passes.
Gas metal arc welding
Gas metal arc welding, often known as GMAW, MIG, or MAG depending on shielding gas and regional terminology, uses a continuously fed wire electrode and shielding gas. A typical package includes a constant-voltage power source, wire feeder, welding gun, contact tips, liner, shielding gas cylinder or bulk gas supply, regulator, and work lead. GMAW can support higher productivity in shop fabrication because the wire is continuously supplied, but it is more sensitive than SMAW to wind and poor gas coverage.
Gas tungsten arc welding
Gas tungsten arc welding, or GTAW/TIG, uses a non-consumable tungsten electrode and normally an inert shielding gas. Filler metal may be added separately. GTAW equipment often includes a precise power source, torch, shielding gas system, foot or fingertip control for some work, and sometimes a water cooler. It is valued for control, low spatter, and clean welds on stainless steel, nickel alloys, aluminum, and thin materials. The trade-off is that it is usually slower and more dependent on operator skill than wire-fed processes.
Flux-cored arc welding
Flux-cored arc welding, or FCAW, uses a tubular wire filled with flux. Some wires are self-shielded, while others require external shielding gas. FCAW equipment resembles GMAW equipment in many setups, but the wire, polarity, drive rolls, and fume control needs may differ. It can be productive on thicker sections and structural work, but the selected wire type must match the base metal, position, mechanical requirements, and work environment.
Power source selection is not only about amperage
The power source is the center of the arc welding equipment package, but selecting one only by maximum amperage is a common mistake. A plant or fabrication shop should also evaluate output range, current type, voltage input, duty cycle, process compatibility, portability, controls, serviceability, and environmental conditions.
Standards matter because welding power sources are industrial electrical products, not ordinary workshop tools. ANSI/NEMA/IEC 60974-1 is an American National Standard for arc-welding equipment power sources. The standard applies to power sources for arc welding and allied processes intended for industrial and professional use, with supply limits and design conditions defined in the standard. The standard was reaffirmed in 2023 in the ANSI listing cited here, making it a useful reference point when comparing professional equipment claims. (webstore.ansi.org)
Duty cycle deserves close attention. It describes how long the equipment can weld at a stated output within a defined cycle before cooling is required. A machine advertised with a high maximum amperage may still be unsuitable for repeated heavy welds if its duty cycle at the required current is low. Buyers should compare duty cycle at the actual welding current, not only at the headline rating.
Input power can also decide whether a machine is practical. A shop machine may be connected to stable three-phase power, while maintenance crews may need equipment that can run from plant outlets or engine-driven generators. For process equipment work, the power source must also match the welding procedure, electrode type, wire size, material thickness, and required weld position.
Consumables, shielding gas, and base metal compatibility
Consumables are not secondary details. Electrodes, wires, filler rods, fluxes, and shielding gases directly affect weld quality, productivity, fume generation, and cost. A complete arc welding equipment specification should therefore cover the consumable system, not just the machine.
For SMAW, the electrode classification must match the base metal, position, current type, and required mechanical properties. Low-hydrogen electrodes may require controlled storage and handling when hydrogen cracking is a concern. For GMAW and FCAW, wire diameter and feedability affect arc stability, deposition rate, and penetration profile. Drive roll type, liner condition, contact tip size, and gun length all influence whether the process runs consistently.
Shielding gas selection is equally important. Argon-rich mixtures, carbon dioxide, helium additions, and inert gases are used differently depending on material and process. For example, GTAW on stainless steel commonly requires clean inert shielding, while many carbon steel GMAW applications use argon-carbon dioxide mixtures. The correct gas flow rate must protect the molten weld pool without causing turbulence or drawing air into the arc zone.
Base metal should guide the equipment decision. Carbon steel fabrication may allow several process choices. Stainless steel work may increase the need for fume control and contamination management. Aluminum requires attention to wire feeding, oxide removal, shielding, heat input, and power source characteristics. When the work involves pressure-retaining parts, corrosive service, or regulated plant equipment, welding procedure specifications and qualified welders may be required under the applicable code or project specification.
Safety and compliance considerations for industrial work
Arc welding equipment creates electrical, optical radiation, heat, fire, gas, and fume hazards. In the United States, OSHA’s general industry welding, cutting, and brazing rules are located in 29 CFR 1910 Subpart Q, and OSHA also maintains specific provisions for arc welding and cutting under 1910.254. These rules are not equipment-buying advice, but they establish safety obligations that should influence how a welding station or maintenance setup is planned. (osha.gov) See also: Storage Systems.
Eye and face protection is a core requirement. OSHA’s eye and face protection standard requires suitable protection where employees are exposed to eye or face hazards, and its welding filter guidance lists protective shade recommendations for operations such as gas metal arc welding, flux-cored arc welding, and arc cutting. In practice, the welding helmet, filter lens, safety glasses, and nearby worker protection should be treated as part of the equipment system, not as afterthoughts. (osha.prod.pace.dol.gov)
Fume control is another major factor. NIOSH notes that welding fume health effects vary with exposure intensity, duration, and the specific metals involved. NIOSH resources identify concerns including manganese in welding fumes and health effects linked to metal fumes, while separate NIOSH engineering guidance discusses local exhaust ventilation for welding operations. This is especially relevant in enclosed fabrication bays, vessel interiors, or maintenance areas with limited air movement. (cdc.gov)
Material choice changes the hazard profile. Welding stainless steel or cutting metals containing chromium can create hexavalent chromium exposure concerns; federal health agencies describe occupational exposure risks for workers who weld or cut chromium-containing metals. Nickel, cadmium, beryllium, lead coatings, zinc coatings, paint, oil residue, and cleaning chemicals can also affect the fume and gas mixture. Before welding used process equipment, the work area should be assessed for residues, coatings, confined-space conditions, and fire or explosion hazards.
Electrical safety should be built into daily practice. Cables, connectors, insulation, electrode holders, torch components, and work clamps should be inspected. Return current paths should be intentional and secure, not routed through bearings, instrumentation, piping supports, or unintended plant components. When welding is paused for a substantial period, OSHA rules for arc welding include removing electrodes from holders and locating holders to prevent accidental contact, along with disconnecting the machine from the power source. (govinfo.gov)
A practical selection checklist for process equipment applications
The following checklist can help narrow the choice of arc welding equipment for fabrication and maintenance tasks without assuming that one process is always superior.
- Define the work type. Is the work new shop fabrication, field installation, emergency repair, overlay, small-bore tubing, structural support, or vessel internals?
- Identify the material. Confirm base metal grade, thickness, coating, cleanliness, and whether corrosion service or pressure service affects the procedure.
- Match the process to the environment. SMAW and self-shielded FCAW may tolerate outdoor conditions better than gas-shielded processes, while GMAW and GTAW often perform best with controlled shielding.
- Check access and position. Pipe, vessel nozzles, internal baffles, and skid frames may limit torch angle, cable routing, and visibility.
- Compare output at real settings. Review amperage range and duty cycle at the current actually needed for the weld, not only the maximum rating.
- Specify consumables and accessories. Include electrodes, wire, filler rods, gases, regulators, torches, liners, tips, drive rolls, clamps, and storage requirements.
- Plan fume and fire controls. Consider local exhaust ventilation, respiratory protection assessment, hot-work permits, fire watch, spark containment, and nearby process hazards.
- Confirm procedure and inspection needs. If work is governed by a code, project specification, or plant integrity program, equipment must support the qualified welding procedure.
For a fabrication shop, the decision may favor GMAW or FCAW equipment when repeatability and deposition rate are central. For field repair, SMAW equipment may remain attractive because it is portable and less dependent on shielding gas. For stainless steel, sanitary, thin-wall, or high-control welds, GTAW may justify its slower travel speed. For many plants, the best answer is not one process but a small set of compatible machines and accessories matched to recurring tasks.
Common specification mistakes to avoid
One mistake is buying a machine before defining the welding procedure. A power source that looks economical can become expensive if it cannot support the required current, polarity, waveform, wire feed system, or duty cycle. Another mistake is ignoring accessories. A poor work clamp, undersized cable, worn liner, incorrect drive roll, or unstable gas regulator can make a capable power source perform poorly.
Another common issue is underestimating the cost of ventilation and protection. Welding inside vessels, near coated steel, or around stainless alloys may require more planning than bench welding in open air. Fume extraction, gas monitoring, respiratory protection evaluation, and hot-work controls can be more important to safe execution than the machine model itself.
Finally, buyers should be careful with vague claims such as “multi-process” or “industrial grade.” Multi-process equipment can be valuable, but only if it supports the exact processes and controls needed for the job. A machine that can perform SMAW, GMAW, and GTAW in a limited way may still be less effective than a dedicated setup for repetitive production welding.
Frequently asked questions
What is the most versatile arc welding equipment for maintenance?
For general plant maintenance, SMAW equipment is often considered versatile because it is portable, relatively simple, and does not require shielding gas. However, versatility depends on the material, weld position, thickness, and procedure requirements. Many maintenance teams also use GMAW, FCAW, or GTAW equipment for specific recurring jobs.
Is MIG welding equipment the same as arc welding equipment?
MIG welding equipment is one type of arc welding equipment. The broader category also includes stick welding, TIG welding, flux-cored welding, submerged arc welding, and other processes. MIG equipment usually includes a power source, wire feeder, welding gun, shielding gas system, and related consumables.
Why does duty cycle matter when selecting a welder?
Duty cycle matters because industrial welding often requires repeated welds at sustained output. If the equipment cannot maintain the required current without overheating, productivity falls and the machine may shut down for cooling. Duty cycle should be compared at the amperage required by the application.
What should be checked before welding process equipment that has been in service?
Before welding used process equipment, the team should confirm the material, previous contents, coatings, cleanliness, isolation, ventilation, confined-space status, fire risk, and applicable repair procedure. Residues, vapors, corrosion products, and coatings can create hazards that are not obvious from the outside.
How should a shop choose between GMAW, GTAW, SMAW, and FCAW?
The choice should be based on weld quality requirements, material, thickness, position, production rate, environment, welder skill, inspection requirements, and safety controls. GMAW and FCAW often support higher productivity, GTAW provides strong control and clean welds, and SMAW remains useful for repair and field work.